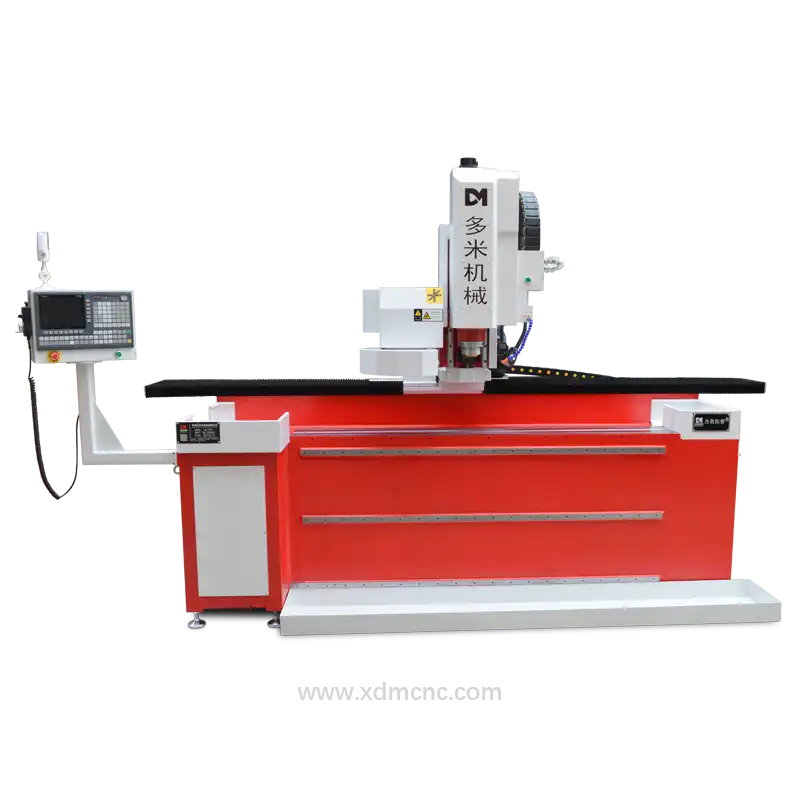
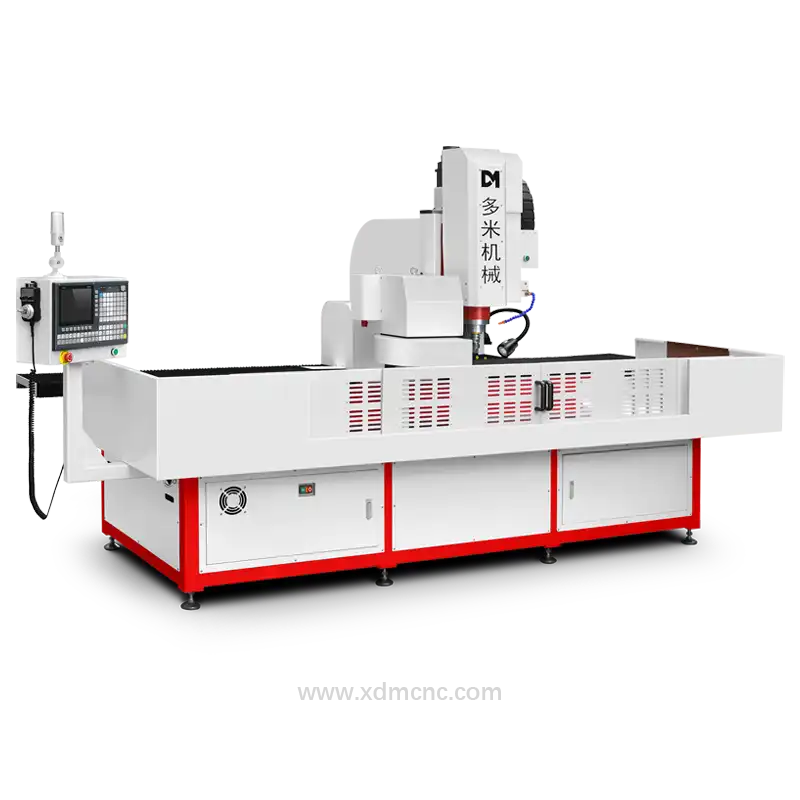
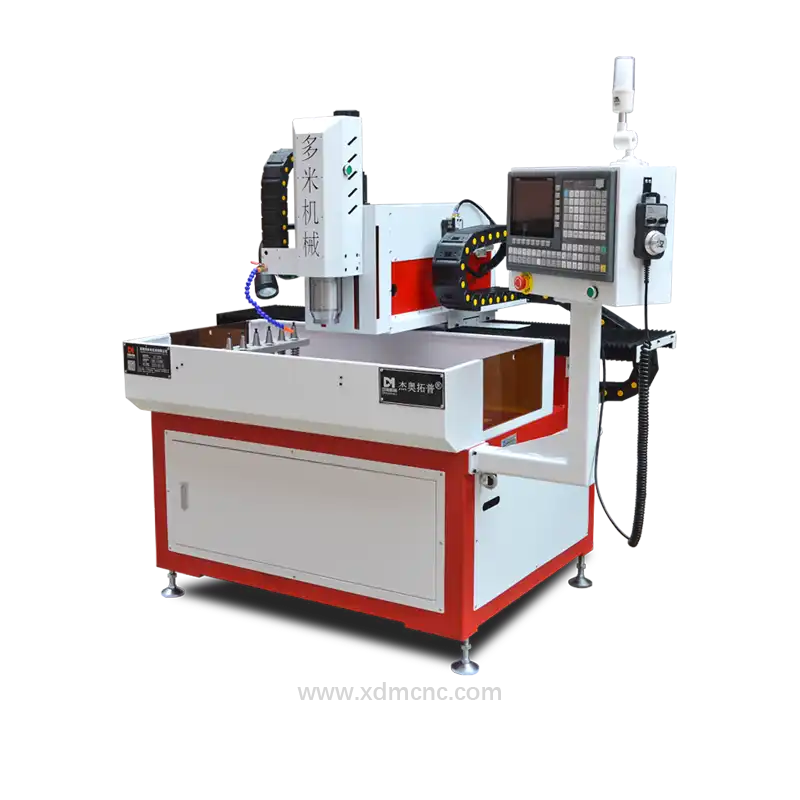
Overview of CNC Drilling of Aerospace Engine Blades
CNC drilling of aerospace engine blades represents one of the most demanding machining processes in contemporary manufacturing. Modern gas turbines and jet engines operate under extreme thermodynamic conditions, with combustor exit temperatures exceeding 1,400°C to 1,650°C—far surpassing the melting point of standard metallic substrates.
To prevent catastrophic thermal fatigue and structural breakdown, high-pressure turbine (HPT) and low-pressure turbine (LPT) blades rely on complex internal cooling channels and thousands of intricate micro-cooling holes. High-precision CNC drilling of aerospace engine blades delivers the positioning accuracy, angular fidelity, and surface integrity required to produce these vital film-cooling features while adhering to rigid aerospace standards such as AS9100 and AMS specifications.
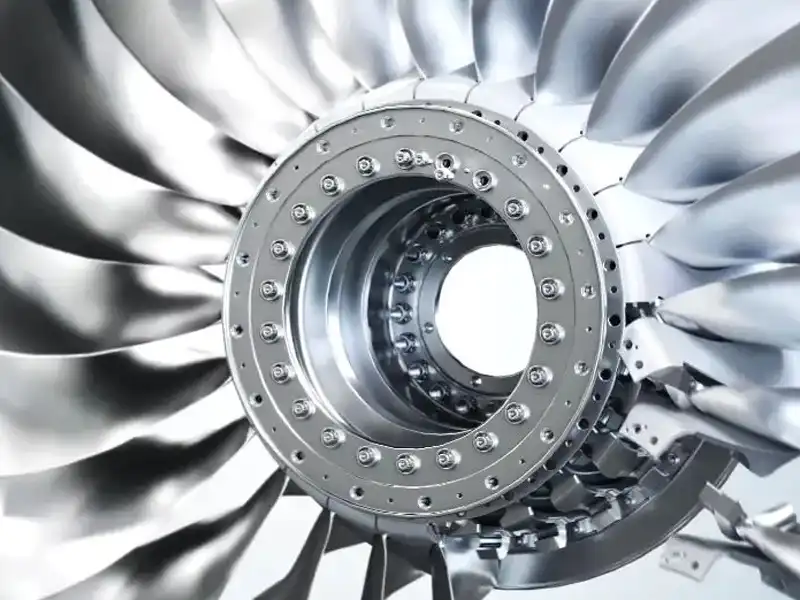 DUOMI CNC Intelligent Manufacturing Solutions for Aerospace Engine Components
Critical Considerations in Turbine Blade Micro-Drilling
1. Film Cooling Hole Design & Aerodynamics
Turbine blade film cooling functions by bleeding pressurized compressor air through internal blade passages and exhausting it across the outer airfoil surface. This creates a boundary layer of cool air that insulates the blade from direct plasma gas flow.
- Micro-Hole Dimensions: Cooling hole diameters typically range between 100 µm and 700 µm (0.1 mm – 0.7 mm), with depth-to-diameter aspect ratios reaching 30:1 or greater.
- Complex Geometry Entry: Advanced film cooling utilizes shaped diffusers (e.g., fan-shaped or laid-back diffuser exit geometries) to maximize cooling coverage. Executing compound-angle entry points demands multi-axis interpolations with angular tolerances tight within ±0.1°.
- Tight Tolerances: Hole spatial positioning must strictly maintain ±0.005 mm to ±0.010 mm to ensure balanced mass flow rates across the entire airfoil profile.
2. Superalloy Compatibility & Coating Integrity
Aerospace turbine blades are cast from advanced heat-resistant materials, including single-crystal (SX) nickel-based superalloys (e.g., CMSX-4, René N5, Inconel 718) and coated with ceramic Thermal Barrier Coatings (TBC) like Yttria-Stabilized Zirconia (YSZ).
- Substrate Hardness & Work-Hardening: Nickel-based superalloys exhibit rapid work-hardening characteristics during cutting. CNC micro-drilling systems require optimized feed-per-tooth parameters and ultra-stiff spindles to maintain continuous chip load without causing tool deflection or micro-fractures.
- Delamination Prevention: Penetrating brittle ceramic TBC layers prior to reaching the metallic substrate presents significant delamination risks. Advanced high-speed CNC peck drilling cycles and specialized PCD diamond-coated tooling protect the ceramic-metallic interface from spalling and micro-cracking.
- Elimination of Recast Layers: Unlike traditional Electrical Discharge Machining (EDM), which leaves a brittle thermal heat-affected zone (HAZ) or recast layer susceptible to micro-fissuring, mechanical CNC micro-drilling delivers smooth hole bore walls without altering material metallurgy.
Technical Advantages of CNC Drilling for Engine Blades
Compared to conventional manufacturing methods, implementing modern CNC drilling of aerospace engine blades yields distinct engineering and operational advantages:
- Superior Hole Quality & Metallurgical Integrity: CNC mechanical micro-drilling eliminates thermal degradation, micro-cracks, and recast layers on critical single-crystal superalloy grain structures.
- Multi-Axis Spatial Versatility: Modern 5-axis and 6-axis CNC machine configurations allow seamless execution of complex compound angles across dynamic airfoil surfaces in a single setup.
- Custom Geometry Machining: CNC micro-milling and spiral interpolation modes allow for customizable diffuser shapes (fan, oval, or teardrop exits) directly integrated into the drilling cycle.
- High Throughput & Tooling Efficiency: Automated tool changers (ATC), real-time tool breakage detection sensors, and high-pressure coolant (HPC) systems operating at 100–150 bar drastically reduce cycle times while prolonging tool life.
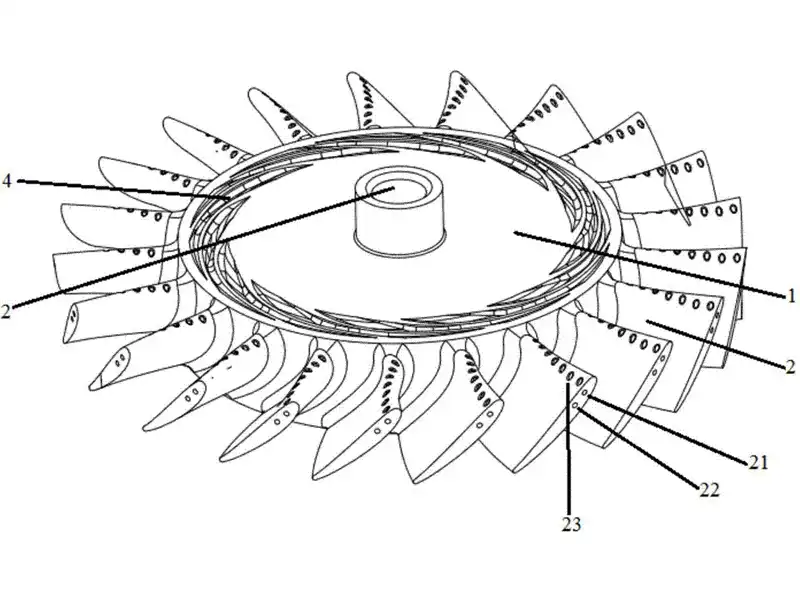 Precision Micro-Drilling of Cooling Holes on Aero-Engine Turbine Blades
Advanced CNC Drilling Innovations & Techniques
High-Speed Peck & Spiral Drilling
Advanced peck-drilling algorithms dynamically adjust retract steps based on real-time torque feedback. This prevents chip packing inside ultra-deep 100 µm micro-bores while ensuring optimal heat dissipation.
Ultra-High Pressure Through-Tool Coolant (HPC)
Injecting synthetic coolant or cryogenic fluids directly through micro-tool channels at pressures exceeding 120 bar flushes micro-chips instantaneously, preventing chip welding and tool breakage in sticky heat-resistant alloys.
Integrated Optical & Automated Inspection
Leading aerospace CNC manufacturing centers combine tactile probing with in-line laser measurement and vision inspection. Systems verify micro-hole position, breakout geometry, and exit hole clean-up before removing the blade fixture.
Process Parameter Specifications
| Process Parameter | Standard Aerospace Target Specification |
|---|---|
| Hole Diameter Range | 0.10 mm – 0.70 mm (100 – 700 µm) |
| Positioning Accuracy | ±0.005 mm |
| Angular Tolerance | ±0.1° |
| Max Aspect Ratio (D:L) | Up to 30:1 |
| Coolant Pressure (HPC) | 100 bar – 150 bar |
| Surface Finish (Bore) | Ra < 0.4 µm |
| Applicable Standards | AS9100 Rev D, ISO 9001, AMS 5666 / AMS 5383 |
Conclusion
The continuous advancement in CNC drilling of aerospace engine blades plays a fundamental role in modern aviation propulsion. By delivering non-thermal micro-hole execution, precise multi-axis compound alignment, and consistent quality under strict aerospace compliance standards, high-precision CNC equipment ensures maximum fuel efficiency and mechanical reliability in demanding thermal environments.
Need High-Efficiency CNC Drilling & Tapping Machinery?
Consult with our senior application engineers to get a custom cycle time simulation and tailored machine proposal within 24 hours.