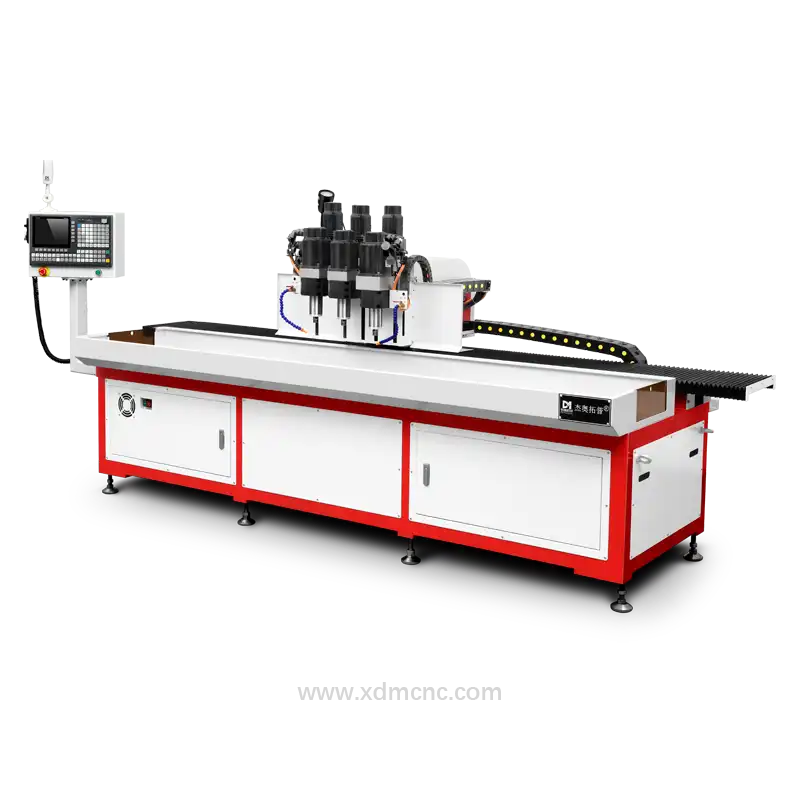
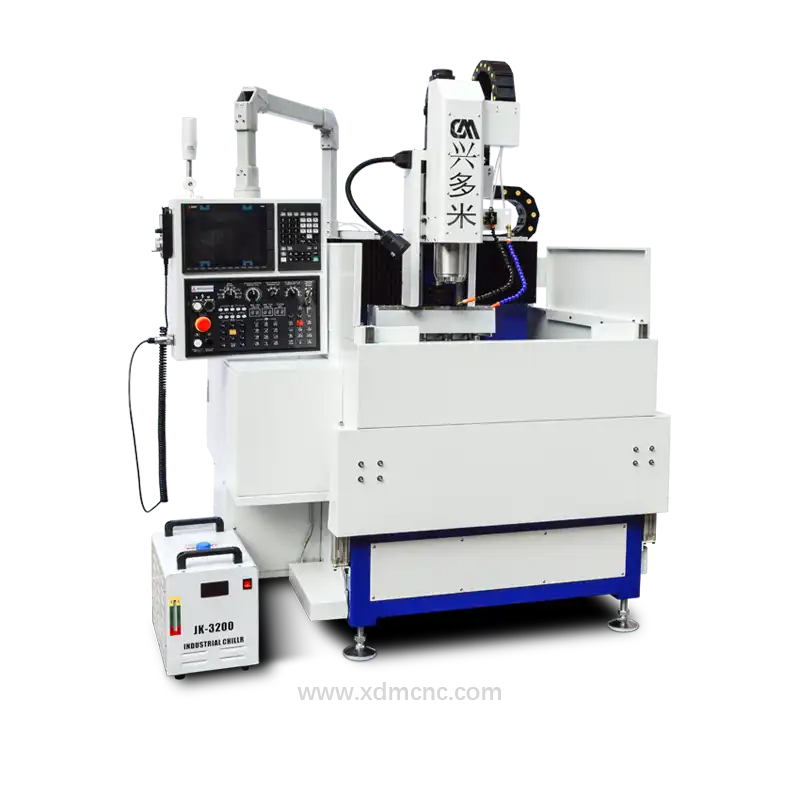
The emergence of new CNC drilling technology applications marks a major leap forward in ultra-precision manufacturing. High-performance industries—such as aerospace propulsion, semiconductor fabrication, solar photovoltaics, flat panel displays, micro-casting, and medical devices—demand unprecedented hole density, tight tolerances, and non-destructive machining on advanced engineered materials.
Historically, aero-engine performance in precision manufacturing has faced technical bottlenecks in material processing technology. The introduction of modern CNC micro drilling machine applications effectively addresses these challenges, enabling high-yield production of micro-structures that were once impossible or cost-prohibitive.
1. Precision CNC Hole Drilling in Aerospace & Propulsion Systems
In gas turbine engines, turbine blades must operate continuously under thermal loads exceeding 1400°C. To prevent structural degradation and melting, aerospace engineers rely on intricate film cooling hole networks to create a protective boundary layer of cooler air over the blade surface.
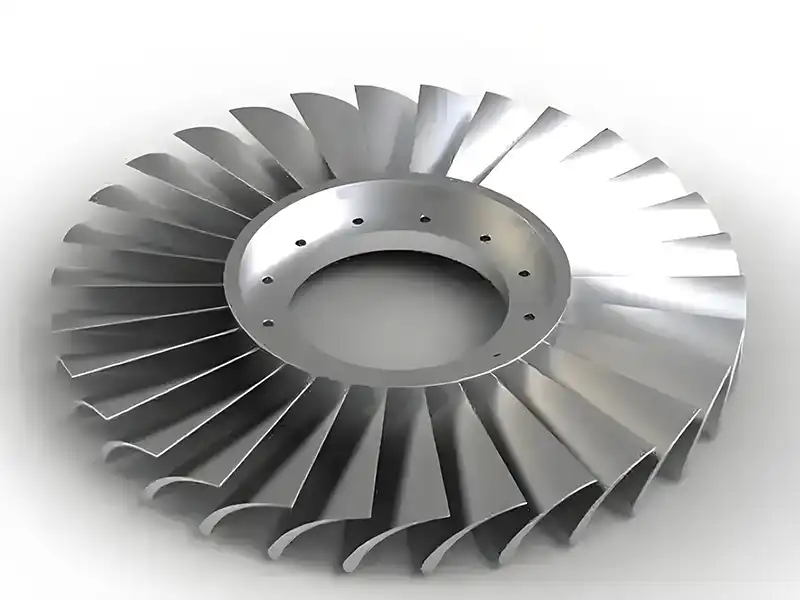
Turbine Blade Micro-Hole Cooling Challenges
- Micro Diameters: Cooling holes typically range from 100 to 700 microns (µm) in diameter.
- Complex Compound Angles: Drilling angles vary from 15° to 90° relative to contoured, curved blade surfaces.
- Non-Circular Geometry: To optimize cooling air coverage, hole geometry often transitions into fan-shaped, trapezoidal, or rectangular diffuser exits.
- Superalloy & Coating Machining: Turbine blades are crafted from nickel-based superalloys (e.g., Inconel 718, René 80) and coated with non-conductive Thermal Barrier Coatings (TBC) like Yttria-Stabilized Zirconia (YSZ).
Why Advanced CNC Drilling Technology Outperforms EDM
While high-speed Electrical Discharge Machining (EDM) was historically utilized for cooling holes, it exhibits severe limitations: 1. Tooling & Wear: High-speed EDM tool electrodes suffer rapid wear, causing dimensional instability. 2. Material Limitations: EDM requires conductive workpieces. It cannot process ceramic TBCs or future non-metallic composite blades without cracking or delamination. 3. Heat-Affected Zone (HAZ): EDM leaves a micro-cracked recast layer, degrading fatigue resistance. 4. Chip Evacuation: Slow spark erosion rates and poor flush/chip removal restrict automated mass production.
Modern CNC drilling solutions overcome these constraints through non-contact or high-rpm mechanical micro-drilling integration. Featuring zero mechanical deformation, position repeatability within ±0.002 mm, and high material adaptability, advanced CNC drilling technology enables clean, burr-free micro-holes across both conductive alloys and insulating ceramic coatings.
Furthermore, through multi-axis CNC system integration and proprietary spiral trajectory drilling algorithms, engineers can custom-machine complex fan-shaped exit geometries directly in a single setup, achieving international leading benchmarks in aerospace hole processing.
2. CNC Micro Drilling Machine Applications in the 3C Electronics Industry
The 3C sector (Computer, Communication, and Consumer Electronics) represents another primary driver for precision micro-hole technology. Modern electronics require ultra-high hole density, high speed, and clean edge quality.
Key 3C Application Areas:
- HDI PCB Micro-Vias: Rapid drilling of high-density interconnect circuit boards with drill diameters below 0.15 mm.
- Wafer Dicing & Semiconductor Processing: Precise micro-hole patterns and slotting on silicon, quartz, and power semiconductor substrates.
- Hard & Brittle Materials: Drilling high-touch consumer components made of synthetic sapphire, chemically toughened glass, ceramics, and graphene.
With smartphones and wearable devices increasingly utilizing scratch-resistant sapphire covers, structural ceramics, and glass backs, standard mechanical punch or press methods are obsolete due to cracking. CNC micro drilling machines offer high rotational speeds (up to 60,000–120,000 RPM), controlled force dynamics, and low thermal transfer, making them an indispensable component of automated 3C processing lines.
3. Technical Comparison: CNC Micro Drilling vs. Traditional Micro-Machining
| Feature / Metric | Advanced CNC Micro Drilling | High-Speed EDM | Conventional Mechanical Drilling |
|---|---|---|---|
| Material Compatibility | Metals, Ceramics, Sapphire, TBCs, Composites | Conductive Metals Only | Soft Metals & Plastics |
| Hole Diameter Range | 100 µm – 3.0 mm | 150 µm – 2.0 mm | > 1.0 mm |
| Positional Accuracy | ±0.002 mm | ±0.010 mm | ±0.050 mm |
| Recast Layer / HAZ | None / Negligible | Present (Requires post-treatment) | None |
| Diffuser / Shaped Holes | Integrated via spiral CNC trajectory | Requires custom electrode shapes | Not Possible |
Summary & Industry Outlook
From enhancing fuel efficiency in next-generation aero-engines to driving ultra-thin glass and wafer processing in consumer electronics, applications of new CNC drilling technology continue to expand rapidly. By integrating multi-axis motion control, real-time tool breakage sensing, and ultra-high-speed spindles, DUOMI CNC delivers precision CNC micro drilling solutions tailored for high-yield, complex industrial manufacturing.
Need High-Efficiency CNC Drilling & Tapping Machinery?
Consult with our senior application engineers to get a custom cycle time simulation and tailored machine proposal within 24 hours.