Best Way to Drill Aluminum: Complete Industrial Machining & Pipe Drilling Guide
Drilling aluminum efficiently demands precise tool geometry, optimized cutting parameters, and effective thermal management. Due to its high thermal conductivity, low melting point, and ductile nature, aluminum alloys (such as 6061-T6, 7075-T6, and 5052) tend to stick to cutting edges—a phenomenon known as Built-Up Edge (BUE). Without proper techniques, this leads to clogged flutes, rough surface finishes, oversized holes, and tool breakage.
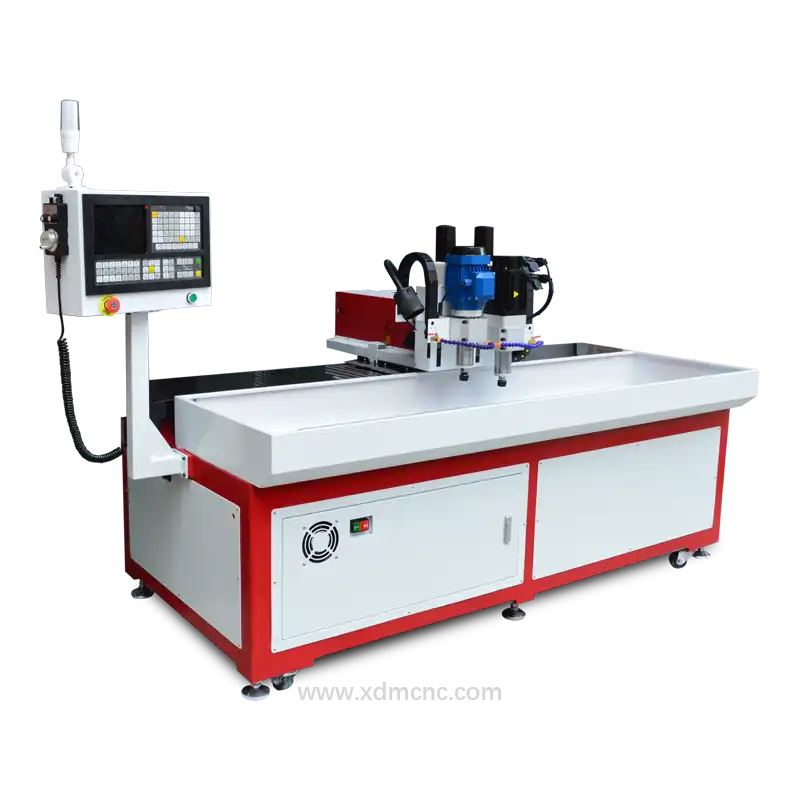
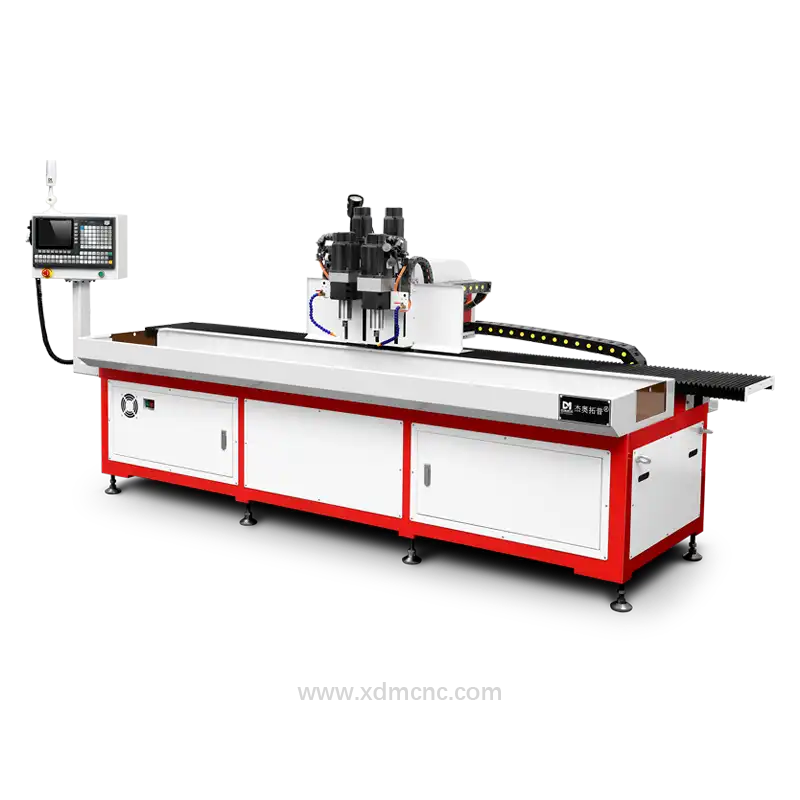
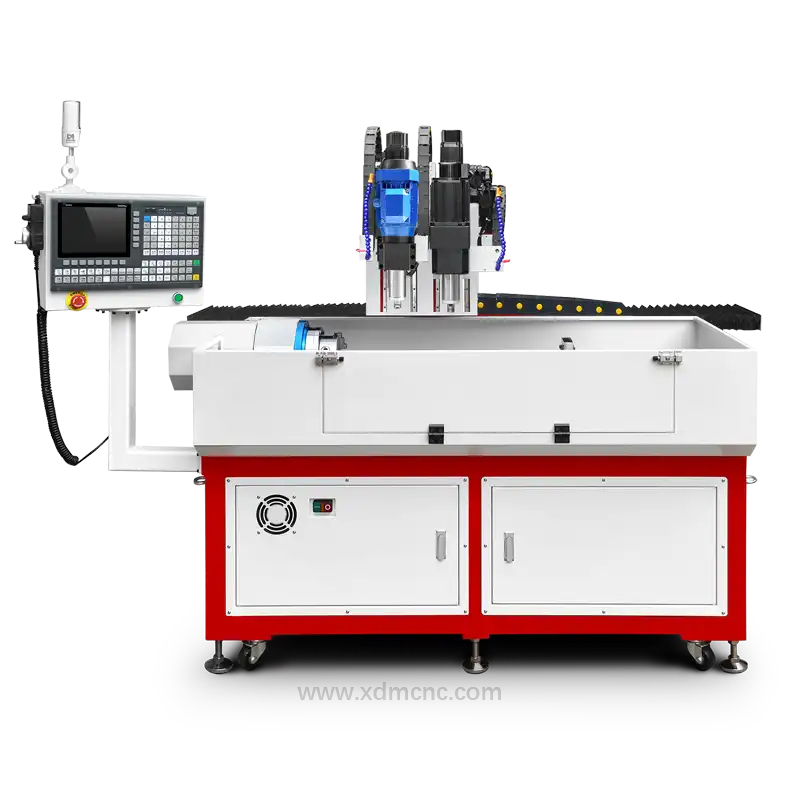
Whether working with sheet metal, extruded structural profiles, or utilizing an automated Aluminum Round Pipe Drilling Machine, following industry-standard parameters ensures clean, high-speed, and burr-free operations.
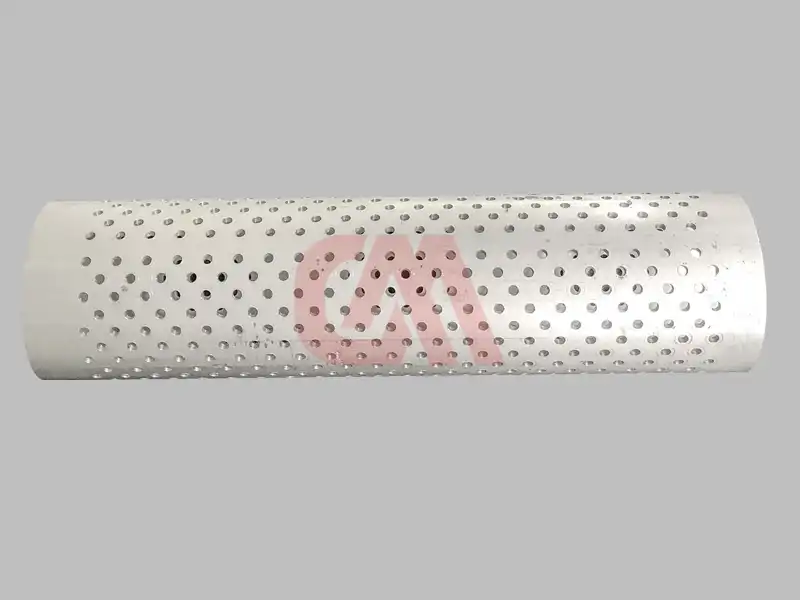 Figure 1: High-speed automated drilling on round aluminum pipe (4 mm Hole Diameter, 3 mm Wall Thickness).
1. Tool Selection: Choosing the Best Drill Bit for Aluminum
Tool geometry and substrate material dictate chip flow and tool life when drilling non-ferrous metals like aluminum.
Recommended Substrates
- High-Speed Steel (HSS & HSS-Co): Excellent toughness for manual operations and general job-shop applications. Cobalt (M35/M42) provides superior heat resistance.
- Solid Carbide: The industry standard for industrial CNC operations. Carbide bits withstand high surface feet per minute (SFM) and maintain sharp cutting edges significantly longer.
- Carbide-Tipped / Indexable Insert Bits: Ideal for production environments and heavy-duty structural pipe drilling.
Essential Tool Geometry Specifications
- Helix Angle: High helix angles (35° to 45°) are recommended to rapidly evacuate continuous, gummy aluminum chips.
- Point Angle: A 135° split point minimizes walking and eliminates the need for center punching in automated setups. For thin-walled tubing, a 118° or modified parabolic flute bit reduces exit burr formation.
- Coatings: Uncoated (bright polish) tools minimize friction with soft aluminum. If coated, use TiB2 (Titanium Diboride) or DLC (Diamond-Like Carbon). Avoid TiAlN coatings, as aluminum reacts chemically with the titanium-aluminum elements in the coating.
2. Speed and Feed Guidelines (RPM & Feed Rate)
Determining the correct cutting speed (SFM) and Surface Speed is critical. Aluminum accepts high speeds, but improper feeds cause friction and tool clogging.
Recommended Cutting Parameters for Standard Alloys (e.g., 6061/6063)
| Tool Diameter (in / mm) | High-Speed Steel (HSS) RPM | Carbide Drill RPM | Feed Rate (in/rev / mm/rev) |
|---|---|---|---|
| 1/8" (3.175 mm) | 3,800 - 5,000 | 8,000 - 12,000 | 0.002 - 0.004 in/rev (0.05 - 0.10 mm) |
| 1/4" (6.35 mm) | 2,000 - 3,000 | 4,500 - 7,500 | 0.004 - 0.008 in/rev (0.10 - 0.20 mm) |
| 3/8" (9.525 mm) | 1,200 - 2,000 | 3,000 - 5,000 | 0.006 - 0.010 in/rev (0.15 - 0.25 mm) |
| 1/2" (12.7 mm) | 900 - 1,500 | 2,200 - 3,800 | 0.008 - 0.012 in/rev (0.20 - 0.30 mm) |
Formula for Spindle Speed: $$\text{RPM} = \frac{\text{SFM} \times 3.82}{\text{Tool Diameter (inches)}}$$ For Aluminum, target SFM ranges from 200–400 SFM for HSS and 600–1500+ SFM for Carbide.
3. High-Efficiency Pipe & Tube Drilling Automation
Drilling thin-walled aluminum round pipes (e.g., 4 mm hole diameter, 3 mm wall thickness) presents unique mechanical challenges: workpiece deflection, tube distortion, and heavy burr formation on inner walls.
Key Benefits of an Automated Aluminum Round Pipe Drilling Machine
- Pneumatic / Hydraulic Clamping: Custom V-block clamping fixtures secure thin-wall tubing without crushing structural walls.
- Multi-Axis Indexing: Automated rotary axes permit precise indexing for radial, multi-hole, or linear pitch patterns.
- Controlled Peck Cycles: High-speed peck drilling routines break stringy chips and inject coolant directly into the cavity.
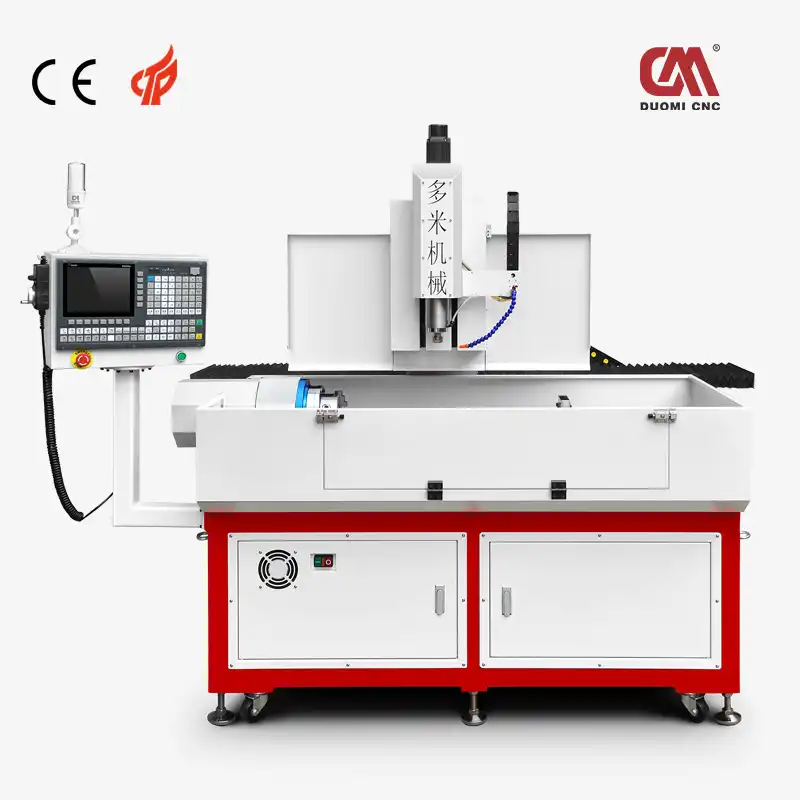 Figure 2: Industrial 4-Axis CNC Pipe Drilling Machine optimized for high-volume aluminum profiles.
4. Lubrication & Cooling Strategies
Cooling is essential when drilling aluminum to break thermal contact and avoid edge welding.
- Water-Soluble Coolant Emulsion (5%-10% concentration): Best for CNC drilling systems; provides continuous washing and chip flushing.
- Minimum Quantity Lubrication (MQL): Uses vegetable-based alcohol oil mist directly targeting the tool tip. Reduces fluid consumption while delivering superior chip clearing.
- Cutting Fluid / Alcohol Spray: Effective for manual setups; isopropyl alcohol lowers local temperatures rapidly without leaving oily residue.
5. Step-by-Step Procedure for Clean, Burr-Free Holes
- Workpiece Setup: Rigidly clamp the aluminum stock to prevent chatter and vibration.
- Center Punch / Spot Drill: Use a 90° or 120° spot drill on CNC equipment (or a center punch for manual drilling) to prevent bit wandering.
- Apply Lubricant: Ensure continuous flow or high-pressure coolant through the tool flutes.
- Execute Peck Cycle: Implement retract peck cycles every 1 to 2 times the drill diameter to drop accumulated chips.
- Deburring: Utilize a 90° countersink or dedicated deburring tool to remove micro-burrs at the entry and exit points.
Summary Checklist for Precision Aluminum Drilling
- Tooling: Bright polish or TiB2-coated carbide bits with 35°–45° high helix.
- Speed/Feeds: High RPM combined with aggressive feeds to ensure cutting rather than rubbing.
- Coolant: High-pressure MQL or flood coolant emulsion.
- Machining: Utilize specialized Aluminum Round Pipe Drilling Machines for high-volume batch processing.
Need High-Efficiency CNC Drilling & Tapping Machinery?
Consult with our senior application engineers to get a custom cycle time simulation and tailored machine proposal within 24 hours.