Graphite materials, renowned for their exceptional electrical conductivity, high thermal resistance (up to 3000°C in inert atmospheres), and chemical inertness, serve as foundational components across lithium battery anodes, electrical discharge machining (EDM) electrodes, and semiconductor single-crystal thermal fields. However, the inherent physical properties of synthetic and natural graphite—specifically low fracture toughness, anisotropic layered microstructures, and abrasive dust generation—present severe obstacles during machining. Modern graphite drilling technology powered by high-precision CNC systems is overcoming traditional process limitations, shifting manufacturing toward zero-defect, highly efficient, and environmentally compliant production.
I. Key Industry Pain Points in Precision Graphite Drilling Technology
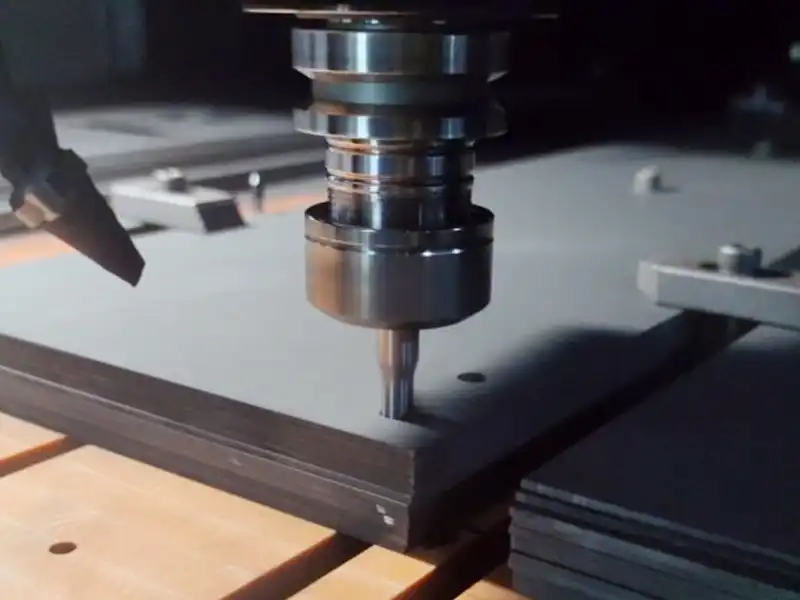
1. Processing Defects Induced by Material Brittleness
- Edge Chipping and Microcracking: Due to weak interlayer Van der Waals forces, conventional graphite drilling technology yields severe entry/exit breakout. Chipping defects often reach 15% to 20% of the nominal hole diameter (e.g., exit chipping >0.45 mm on a φ3.0 mm hole). In EDM electrode fabrication, such edge defects degrade discharge stability and reduce erosion efficiency by up to 30%.
- Delamination in High-Aspect-Ratio Holes: When deep-hole aspect ratios exceed 5:1, conventional axial thrust forces trigger internal step-like delamination, yielding surface roughness values exceeding Ra 3.2 μm.
2. Tool Wear and Degradation Mechanisms
- Extreme Abrasive Wear: Hard inclusions (such as residual silicon carbide, SiC, or metallic impurities) cause rapid micro-chipping and flank wear on cutting edges. Uncoated solid carbide drill bits frequently fail after drilling fewer than 500 holes—less than 10% of their operational lifespan in standard structural steel.
- Thermal Adhesion & Chip Evacuation Failure: At cutting zone temperatures exceeding 200°C, fine graphite micro-powders compact inside drill flutes. This creates severe chip packing (>40% flute blockage rate), drastically increasing torsional torque and leading to catastrophic tool failure.
3. Dimensional Inaccuracy and Geometry Errors
- Taper and Runout Deviations: Deep-hole drilling in hydrogen fuel cell bipolar plates or semiconductor thermal components often suffers from drill walk and taper errors ranging from 0.05 mm to 0.10 mm, disrupting homogeneous gas or fluid diffusion.
- Positional Drift: Spindle vibration and thermal extension can push hole location tolerances outside strict semiconductor requirements (±0.005 mm).
4. Severe Environmental, Health, and Safety (EHS) Risks
- Combustible Dust Explosion Hazards: Graphite fine dust exhibits a low explosion threshold (Lower Explosive Limit, LEL, around 60 g/m³). Uncontrolled dust accumulations pose acute industrial hazard risks.
- Occupational Health Impact: Airborne graphite particles smaller than 5 μm present severe respiratory risks (pneumoconiosis). Conventional wet coolant systems generate hazardous graphite slurry, whereas standard dry exhaust filters often demonstrate sub-90% filtration efficiency.
II. High-Precision CNC Innovations in Graphite Drilling Technology
1. Dynamic Precision Compensation and Motion Control
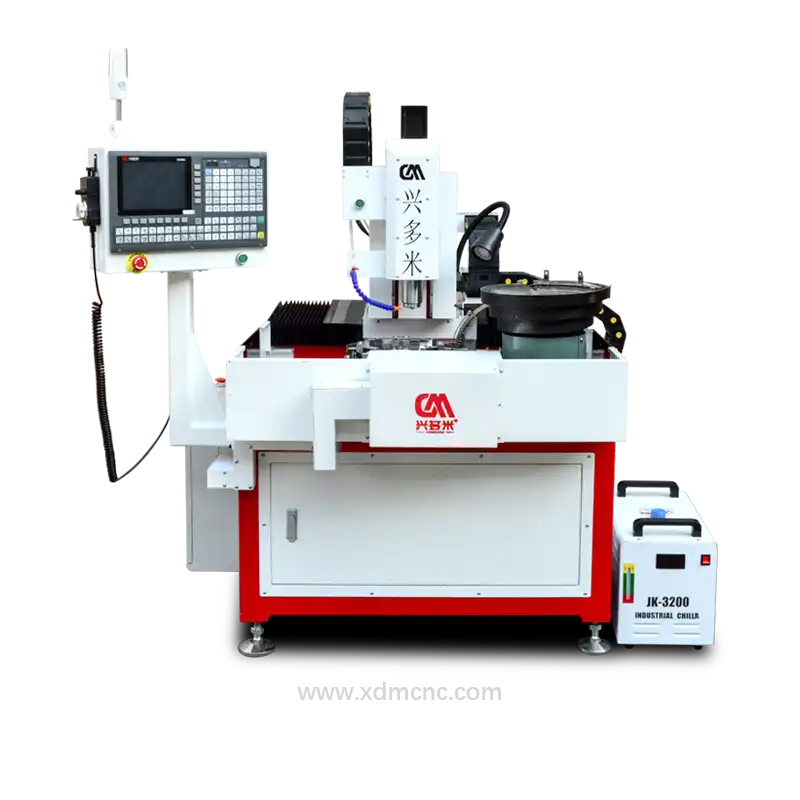
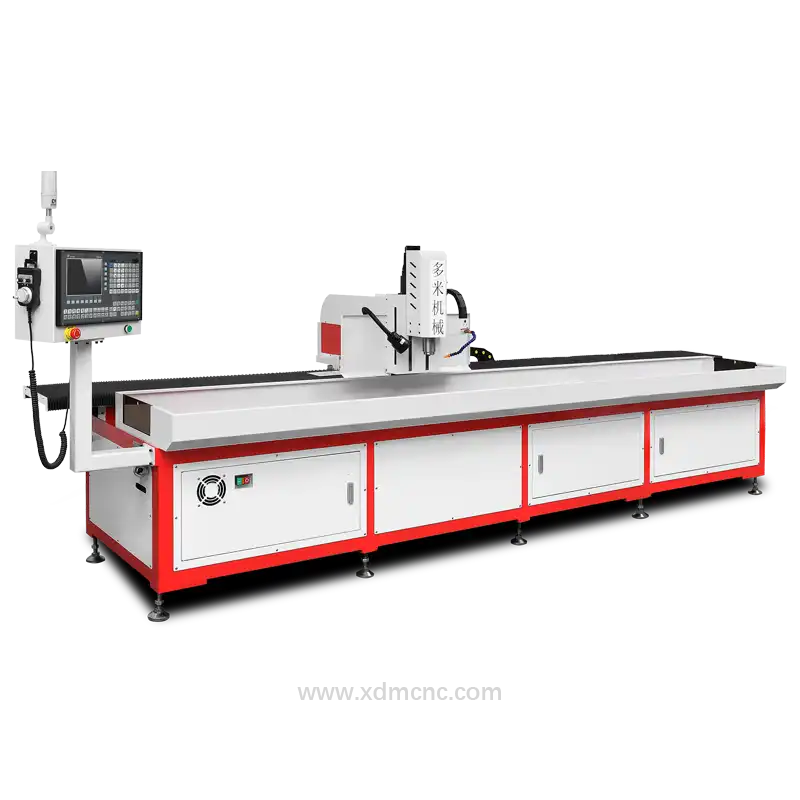
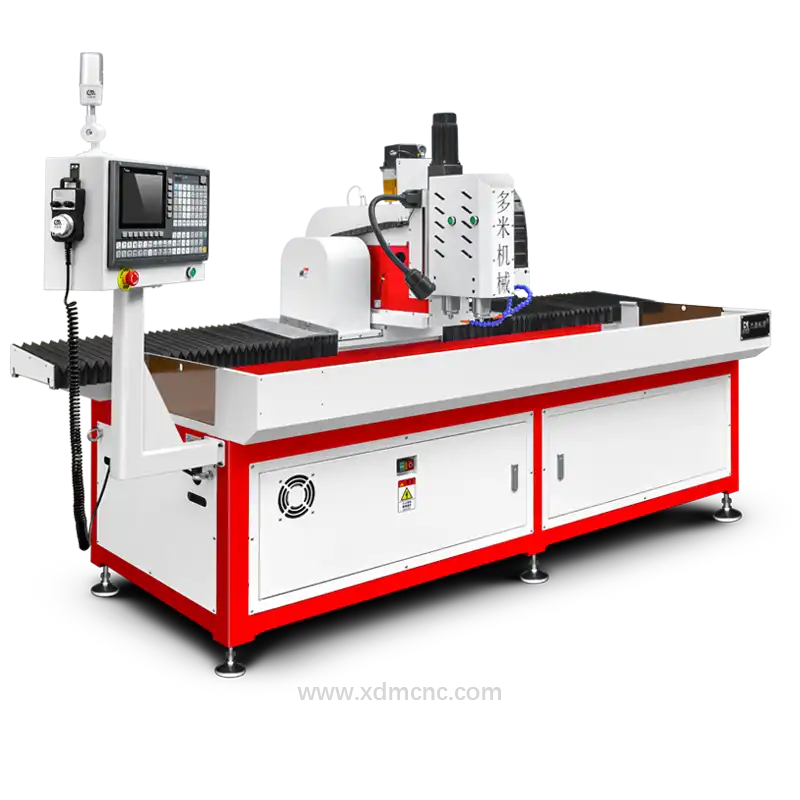
Modern CNC centers designed for specialized graphite drilling technology integrate high-resolution closed-loop feedback systems: * Sub-Micron Encoder Feedback: Nano-scale linear optical scale grating feedback ensures absolute positioning accuracy within ±1.0 μm. * Active Vibration Suppression Algorithms: High-speed spindles utilizing dynamic balancing reduce radial runout to under 0.5 μm at rotational speeds up to 30,000 RPM. * Micro-Hole Realization: Industrial DUOMI CNC drilling machines achieve exit edge chipping under 0.02 mm in micro-hole operations (φ0.5 mm), making high-density pattern drilling viable for lithium battery anode current collectors and fuel cell flow plates.
2. Adaptive AI-Driven Feed Rate & Parameter Optimization
- Real-Time Material Density Sensing: Machine learning models monitor motor load, torque fluctuations, and acoustic emissions to detect local graphite density variations (1.50 to 1.90 g/cm³) and grain sizes (5 to 20 μm).
- Dynamic Cutting Speed Control: CNC controllers dynamically adjust spindle speeds (8,000–30,000 RPM) and feed rates (0.5–5.0 μm/rev), preventing micro-fractures during breakthrough and extending total cutting tool lifespan by over 200%.
3. Integrated Vacuum Extraction & Dry Dust Management
- Positive Pressure Air Curtain Containment: High-velocity air jets create an isolation boundary around the spindle noise cone, reducing dust escaping into the cabin enclosure to under 5%.
- Multi-Stage HEPA & Electrostatic Filtration: Combined electrostatic precipitators and H14-class HEPA filtration systems capture particulate matter down to 0.3 μm with >99.97% efficiency.
- Cleanroom Compliance: Advanced DUOMI DNC series specialized graphite CNC centers limit ambient shop-floor particulate levels to <1.0 mg/m³, fully satisfying OSHA and EU-OSHA airborne exposure standards.
4. Specialized Tool Materials, Coatings, and Micro-Geometries
| Tool Specification / Parameter | Standard Carbide Drill | DLC-Coated Micro-Drill | CVD Diamond-Coated Drill |
|---|---|---|---|
| Friction Coefficient (vs. Graphite) | ~0.60 | ~0.15 | ~0.10 |
| Thermal Resistance Limit | 500°C | 600°C | >800°C |
| Average Tool Life (Holes) | < 500 | 2,500 - 4,000 | > 10,000 |
| Flute Geometry Optimization | Standard 30° Helix | Double-Helix Polish Flute | Parabolic Variable Helix |
| Primary Application Target | Roughing / General Use | Fine EDM Electrodes | High-Volume Anode Plates |
- CVD Diamond & DLC Coatings: Micro-crystalline diamond coatings lower friction, resist extreme abrasion, and retain sharp cutting edge radii (<3 μm) over extended operational cycles.
- Self-Centering Geometry: Dual-angle point designs eliminate lateral drill walk, keeping total concentricity errors within 0.005 mm without requiring center-drilling pre-operations.
III. Industrial Applications of Advanced Graphite Drilling Technology
1. Lithium-Ion Battery Anode Plate Processing
- Technical Goal: Precision micro-drilling of φ0.8–1.5 mm through-holes across porous (30%–50% porosity) artificial graphite sheets (1.2 mm thickness) to optimize electrolyte wetting and lithium-ion diffusion rates.
- Performance Outcome: Dedicated high-speed DUOMI CNC multi-spindle drilling platforms achieve continuous output rates reaching 150 holes/min while maintaining strict dust containment below 0.5 mg/m³.
2. EDM Electrode Fabrication for Aerospace & Automotive Dies
- Technical Goal: High-density matrix drilling of narrow flushing channels in ultrafine grain (grain size <5 μm) high-density graphite blocks.
- Performance Outcome: Eliminates macro-chipping on delicate thin-wall fins, ensuring EDM discharge gap consistency and improving downstream mold spark-erosion speeds by 30%.
3. Semiconductor Thermal Field Component Manufacturing
- Technical Goal: Deep-hole drilling in high-purity isotropic graphite heaters, susceptors, and single-crystal CZ furnace heat shields.
- Performance Outcome: Holds hole straightness and taper errors under 0.02 mm across aspect ratios exceeding 8:1, preventing thermal leakage and ensuring uniform temperature distribution across silicon ingot pulling zones.
IV. Optimized Cutting Parameters for Graphite Drilling Technology
To achieve maximum tool life and minimal edge chipping, technical operators should adhere to the following optimized parameters:
- Peripheral Cutting Speed ($V_c$): 120–250 m/min for diamond-coated carbide tools.
- Feed per Revolution ($f_n$): 0.002–0.015 mm/rev (reduce feed rate by 50% during entry and breakthrough phases).
- Flushing & Dust Control Strategy: Dry cutting accompanied by high-pressure internal air blast (6–8 bar) through tool coolant channels combined with point-of-cut vacuum suction cups (>25 m/s air speed).
- Tool Maintenance Cycle: Monitor high-frequency spindle current signature; replace or re-coat bits when flank wear ($VB$) exceeds 0.15 mm to prevent sudden catastrophic workpiece delamination.
Need High-Efficiency CNC Drilling & Tapping Machinery?
Consult with our senior application engineers to get a custom cycle time simulation and tailored machine proposal within 24 hours.