For thin-walled sheet metals, square tubes, and tubular frames, creating strong and durable internal threads has historically been a major fabrication bottleneck. Conventional fastening methods—such as blind rivet nuts (nutserts), clinch nuts, and welded boss nuts—require multi-step manual assembly, increase raw material costs, and pose severe defect risks such as rivet spin-out during bolt tightening or weld spatter contamination.
Flow drilling (also known as thermal friction drilling or Formdrill) provides an advanced, single-setup thermo-mechanical alternative. By utilizing high rotational speed and controlled axial pressure, frictional heat locally plasticizes the workpiece metal, allowing the conical tool to extrude a solid, monolithic bushing directly from the parent material without producing chips.

Figure 1: High-speed flow drilling and extrusion cycle forming a structural threaded boss on steel tubing.
The Science of Flow Drilling: 4-Step Forming Cycle
The flow drilling process relies on plastic deformation at elevated temperatures (typically 600°C–800°C) rather than material cutting. This rapid cycle takes only 2 to 6 seconds per hole:
- Contact & Frictional Pre-Heating: A solid tungsten carbide conical tool contacts the metal surface at high spindle speeds (1,500 to 4,000 RPM). The axial thrust and friction rapidly heat the contact area to its plasticizing temperature in less than 1 second.
- Material Displacement & Penetration: As the workpiece softens (without reaching its melting point), the tool pushes through the material under controlled CNC feed, displacing plasticized metal both upward and downward.
- Bushing Extrusion: The downward displacement creates a cylindrical collar or bushing whose total wall thickness is 2.5 to 3.5 times the original sheet thickness, providing ample depth for full thread engagement.
- Cold Form Tapping (Chipless Rolling): A fluteless cold-forming tap (roll tap) is subsequently driven into the formed bushing. Instead of cutting fibers and generating chips, it cold-rolls the internal threads, work-hardening the metal grain structure for maximum fatigue strength.

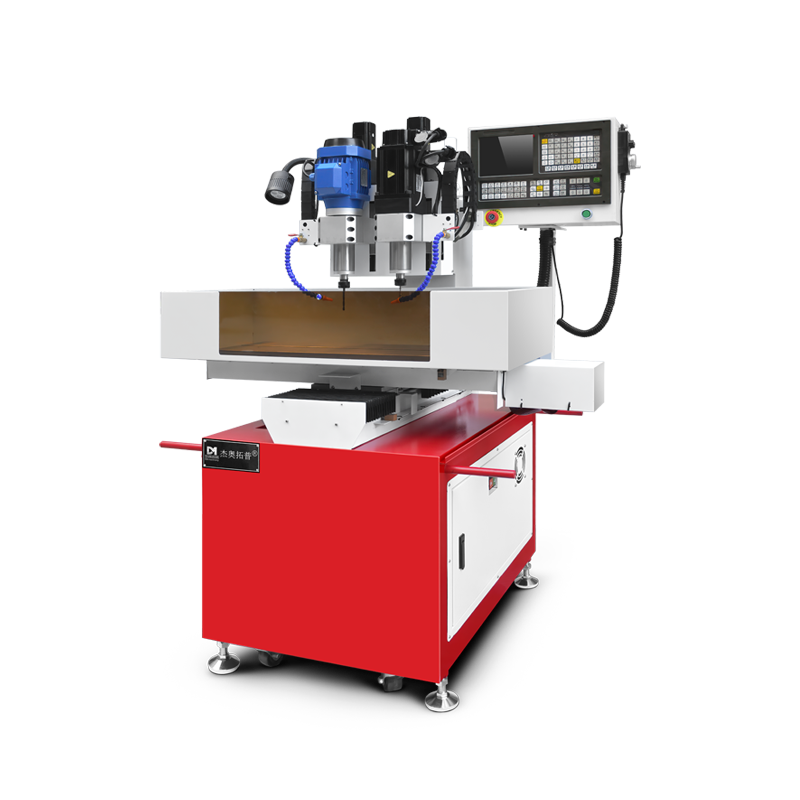
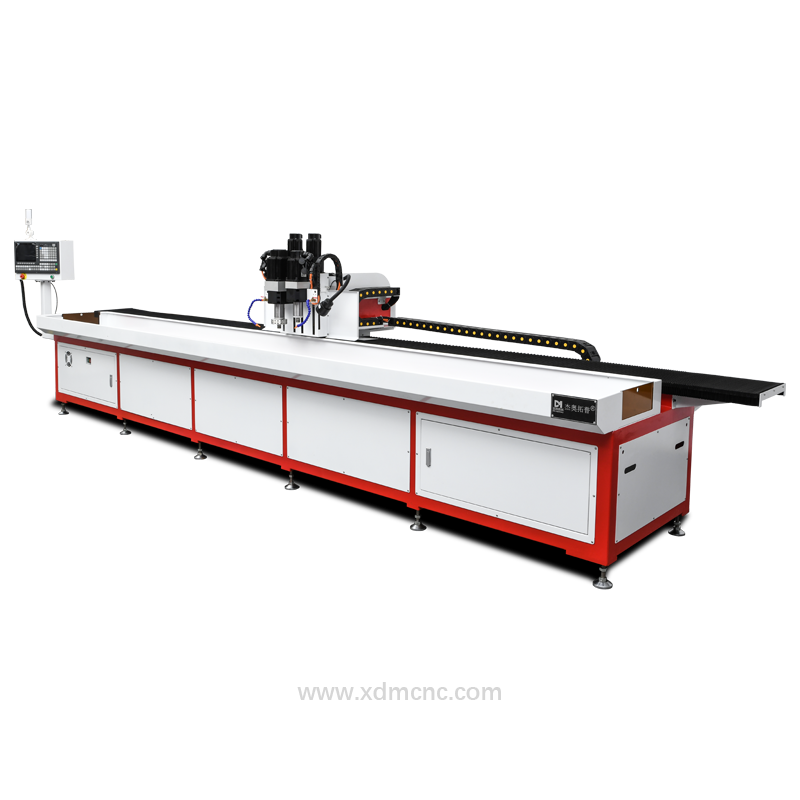
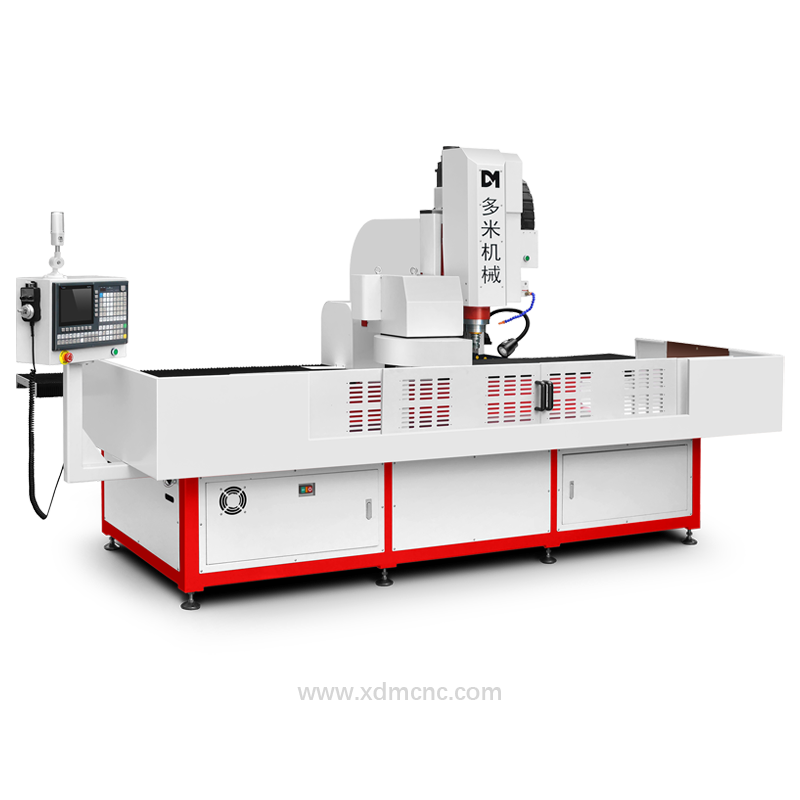
Figure 2: DUOMI high-speed CNC flow drilling and tapping center designed for continuous profile processing.
Recommended CNC Machining Parameters for Flow Drilling
To ensure maximum tool life (5,000 to 15,000 holes per carbide bit) and maintain ISO/DIN standard thread engagement, flow drilling requires rigid CNC equipment and precise speed-feed control:
| Parameter | Typical Operating Range | Engineering Notes |
|---|---|---|
| Workpiece Wall Thickness | 0.8 mm – 12.0 mm | Ideal for 1.2 mm – 4.0 mm tubular profiles |
| Spindle Speed (RPM) | 1,500 – 4,000 RPM | Smaller diameters require higher RPM (e.g., M4 at 3,500 RPM) |
| Process Cycle Time | 2 – 6 seconds / hole | Complete flow drilling and tapping in under 5 seconds |
| Frictional Zone Temperature | 600°C – 800°C | Softens metal without phase destruction or melting |
| Tool Material | Micro-grain Tungsten Carbide (WC-Co) | High heat resistance and extreme wear durability |
| Bushing Length Gain | 2.5x – 3.5x sheet thickness | E.g., a 1.5 mm tube wall forms a 4.5 mm thread boss |
| Lubrication / Paste | High-temp release paste | Applied every 4–5 holes to prevent metal adhesion |
Technical & Economic Comparison: Flow Drilling vs. Rivet Nuts & Weld Nuts
Why are automotive frame manufacturers and metal fabricators transitioning to flow drilling? The comparison matrix below highlights the quantifiable production benefits:
| Evaluation Metric | Flow Drilling & Tapping | Blind Rivet Nuts (Nutserts) | Welded Nuts |
|---|---|---|---|
| Total Cycle Time | 2 – 6 seconds (fully automated CNC) | 15 – 30 seconds (drill + manual insert) | 30 – 60 seconds (weld + slag cleanup) |
| Hardware Fastener Cost | $0.00 (formed from parent metal) | $0.05 – $0.25 per fastener insert | Cost of nuts, filler wire & shielding gas |
| Spin-Out Risk (Torque) | 0% spin risk (monolithic parent metal) | High risk during high-torque tightening | Medium risk from cold welds or fatigue |
| Internal Chips / Burrs | 100% Chip-free (clean inside tube) | Chips created during pre-drilling | Swarf, weld spatter & toxic fumes |
| Pull-Out Strength | 30%–50% higher than inserts | Limited by thin collar flange | Dependent on manual operator skill |
| Automation Suitability | 100% single-setup CNC integration | Requires specialized robotic pop-riveters | Requires dedicated robotic welding cell |
Workpiece Material Compatibility
The flow drilling process is versatile across virtually all ductile ferrous and non-ferrous engineering metals:
- Mild & Structural Steels: S235, S355, AISI 1018, Q235, Q345. Excellent ductility and rapid thermal response.
- Stainless Steels: AISI 304, AISI 316, AISI 430. Flawless bushing extrusion using high-temperature carbide paste.
- Aluminum Alloys: 6061-T6, 6063-T5, 5052. Special flat-collar tooling and lubrication prevent alloy galling.
- Copper & Brass Alloys: Ideal for HVAC manifolds, heat exchangers, and cooling tubes without brazed fittings.
- Pre-Coated & Galvanized Tubes: Extrudes cleanly without destroying adjacent protective surface layers.
Industrial Applications of Flow Drilling Machinery
- Automotive & EV Chassis: Battery tray enclosures, shock-absorber brackets, seat sliders, and tubular bumpers.
- Commercial Fitness Equipment: Heavy-duty structural joints in 40x80 mm and 50x100 mm steel tubing subjected to dynamic loads.
- HVAC & Liquid Cooling Systems: Branch connections on thin-walled copper/brass manifolds without soldered T-pieces.
- Architectural Metalwork & Furniture: Stainless steel balustrades, door frames, and modular tubular racks.
DUOMI High-Speed CNC Flow Drilling Solutions
Implementing industrial flow drilling requires high spindle rigidity, high-torque high-speed motors, and synchronized rigid tapping.
DUOMI CNC Flow Drilling & Tapping Centers feature BT40/BT50 rigid spindles (up to 4,000 RPM), rapid servo reversal for roll tapping, 16–24 station automatic tool changers (ATC), and bed lengths up to 6,500 mm—enabling seamless, multi-station machining for tubes and profiles in one clamping setup.
Need High-Efficiency CNC Drilling & Tapping Machinery?
Consult with our senior application engineers to get a custom cycle time simulation and tailored machine proposal within 24 hours.