MINIMAL FOOTPRINT. MAXIMAL FIREPOWER.
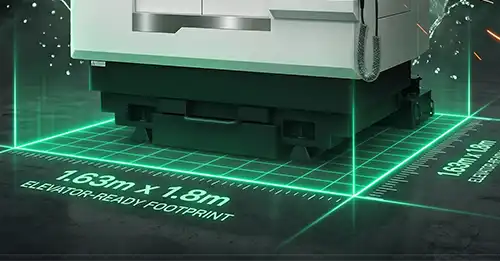
70 N·m BT40 Box-Way muscle packed into a 1.63 × 1.8m elevator-ready frame. Tear through 304 SS with a Ø60mm U-Drill.
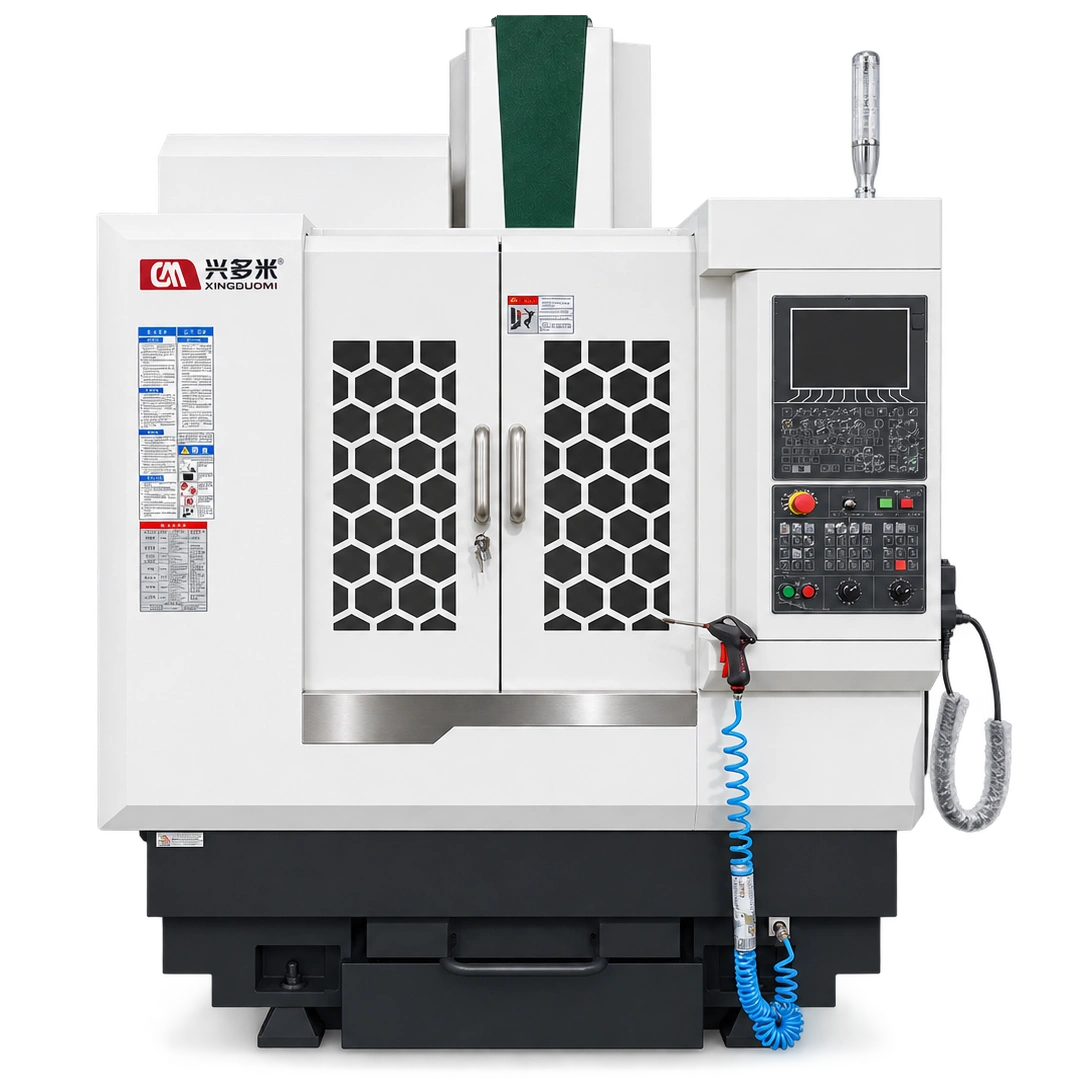
Monolithic Box-Way Architecture: Built for Severe Metal Removal
Click or hover any structural node to inspect specifications. Engineered with Yunnan HT300 cast iron, hand-scraped Turcite-B slideways, and BT40 70 N·m spindle muscle.
Heavy-duty BT40 spindle delivering 70 N·m continuous torque—2× standard BT30. The short-throat headstock (430mm spindle center-to-column) eliminates toolhead leverage deflection under severe radial cutting loads.
High-frequency induction-hardened rectangular box ways paired with imported Turcite-B anti-friction lining. Hand-scraped by master craftsmen to 18–22 contact points/in² with dedicated micro oil-retaining pockets.
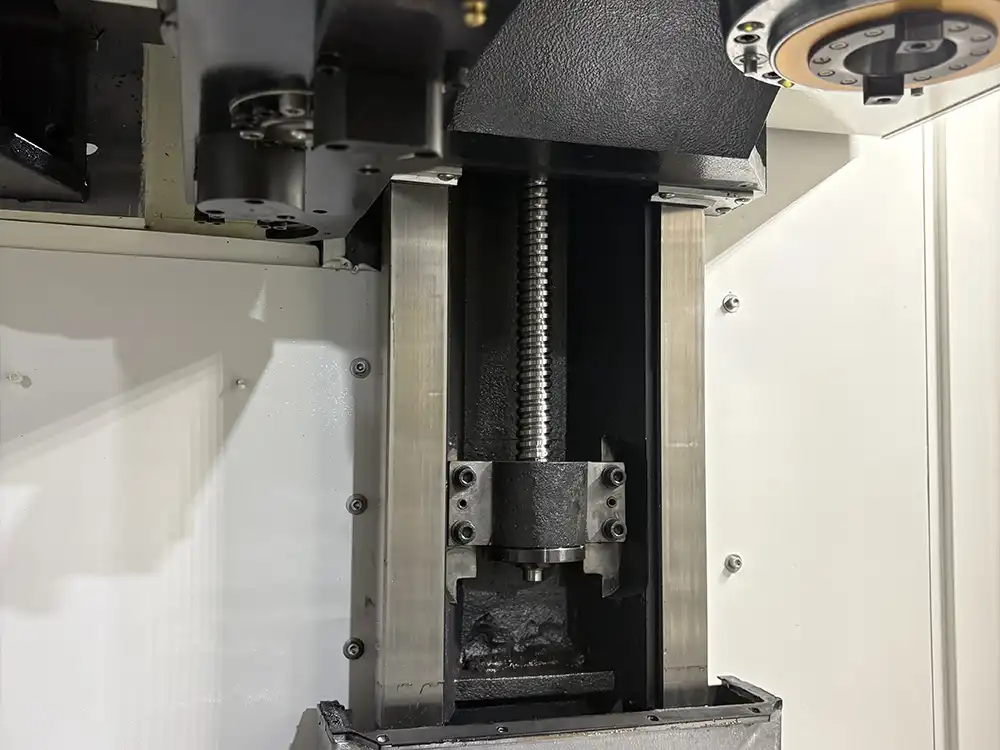
Oversized #35 high-rigidity roller linear guideways deliver 36 m/min agile positioning with high line-contact load capacity. Driven by Taiwan C3 pre-tensioned ball screws and 30% higher torque high-inertia AC servos.
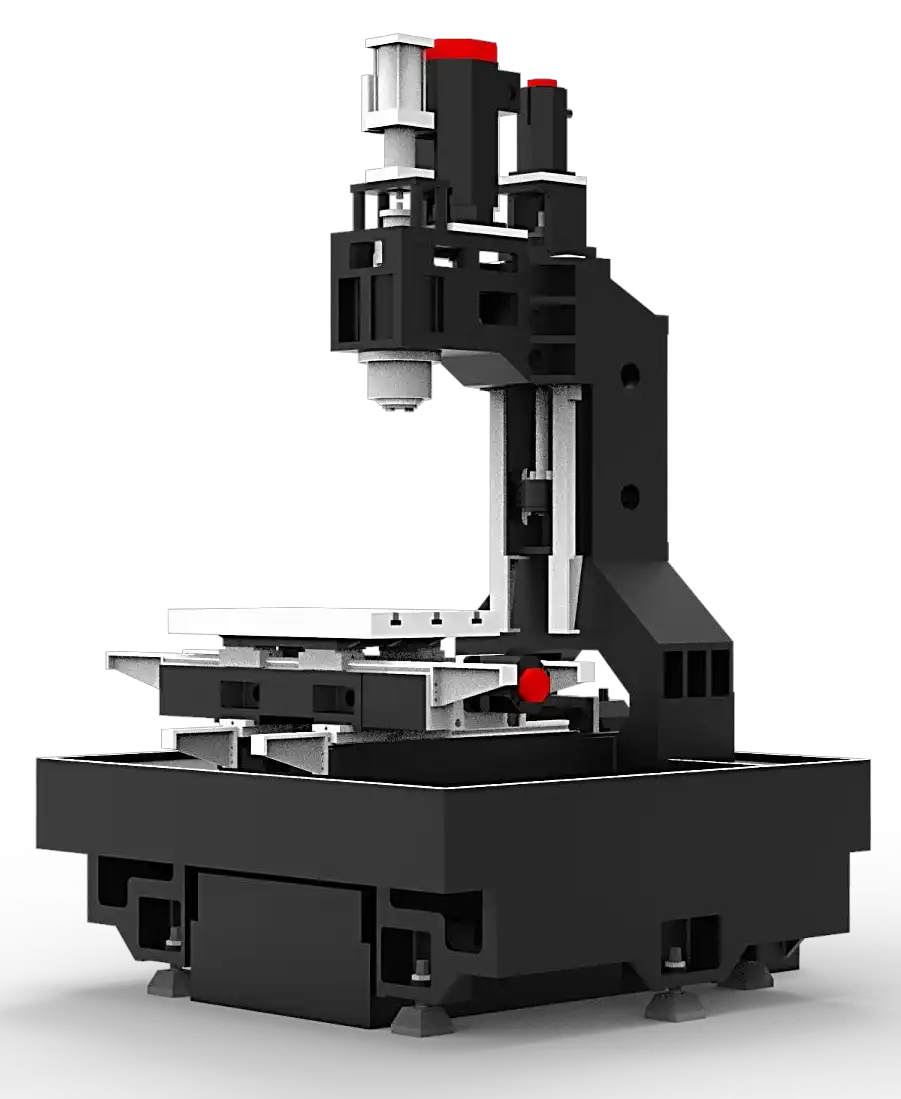
Cast entirely from Yunnan high-density pearlite HT300 gray iron. Subjected to two electric-furnace stress-relief cycles (at 550°C and 600°C) with wide-span A-frame column geometry and dense diagonal cross-ribs.
Extended 750×400mm surface ground worktable supporting up to 300kg workpiece load. Accommodates dual hydraulic clamping vises, large multi-cavity fixtures, or an integrated CNC 4th-axis rotary table.
Coolant collection troughs and steep chip-shedding slopes are integrally cast directly into the heavy monolithic base—zero welded sheet metal joints. Chips and high-volume 30-bar CTS coolant drop directly into the rear bin.
Tough Materials, Severe Tolerances: Proven Field Workpieces
Representative Field Benchmarks — Not Limited to These 3 Industries. Built with 70 N·m spindle torque and vibration-damping box ways, the XDM-V540 excels across all severe metal-removal tasks, including titanium alloys, mold steels, and heavy engineering components.
Stainless Steel 304/316 Valve Bodies
High-torque BT40 cavity milling, deep-hole U-drilling of fluid passages, and rigid tapping of M16 pipe threads with zero tool chatter.
Sanitary Fittings & Heavy Manifolds
Multi-sided boring and deep drilling on brass, bronze, and duplex stainless manifolds where tight bore concentricity is required.
Hydraulic Blocks & Tool Holders
Heavy face milling and deep internal oil circuit drilling in 42CrMo and S45C carbon steels with high chip load without spindle drop.
STOP COMPROMISING. ONE MACHINE TO CRUSH TWO MARKET TRAPS.
Stop choosing between “Too Big for Your Building” and “Too Weak for Your Steel.” Discover how asymmetric hardware engineering eliminates the two greatest false choices in small-part manufacturing.
The Market Trap: Two Flawed Extremes in Small-Part Milling
Why Buyers Lose MoneyCuts tough steel effectively, but weighs over 5 tons and eats 7.0 m² of shop floor. Cannot fit standard factory freight elevators, locking you out of upper-floor facilities and doubling square-meter workshop rental overhead.
Fits elevators and saves space, but spindle torque peaks at only 25–35 N·m with flimsy ball rails. Stalls instantly in 304 stainless steel with violent chatter, poor surface finishes, and chronic carbide insert breakage.
Locked Out of Upper Floors & Bloated Rent Costs
Weight exceeds 3-ton standard factory freight elevators, requiring high-cost ground floor crane installation. Exterior chip conveyors and rear water tanks stick out 2.8m, blocking vital workshop aisles and doubling square-meter rental costs.
Enters 3-Ton Freight Elevators; Fits 50% More Machines
Guaranteed to roll directly into standard 3,000kg freight elevators for effortless upper-floor setup. Integrated tiered vertical chip drop dumps swarf straight down into rolling carts with zero exterior overhang, packing 50% more machining capacity into the exact same floor area.
Chokes in 304 Stainless Steel; Chronic Tool Breakage
Lightweight BT30 high-speed spindles lack low-end torque. Point-contact ball linear guides have minimal vibration damping; the instant a large drill touches 304/316 stainless or alloy steel, violent chatter destroys surface finishes and shatters expensive carbide tips.
2× Brutal Cutting Torque; 90% Vibration Damping
Direct belt-driven BT40 spindle unleashes 70 N·m peak torque. Hand-scraped Turcite-B rectangular box ways provide immense surface-sliding friction, absorbing 90% of drilling impact shock to drive an Ø60mm U-Drill straight through steel in a single continuous cut.
Iron Swarf Jamming; Slow Peck Retractions
External coolant nozzles cannot penetrate deep holes or valve cavities. Hot stringy swarf wraps around the drill body, forcing operators to program slow pecking cycles (Peck Drilling) with constant tool retractions, quadrupling cycle times and risking tool explosion.
5D Deep Holes in a Single Pass; 3× Cycle Speed
Standard 30-Bar high-pressure fluid jets straight through the tool tip directly to the bottom of the cavity. Swarf is continuously blasted backwards out of the hole, enabling single-pass U-drilling up to 5D depth without a single peck retraction, speeding up production by 3×.
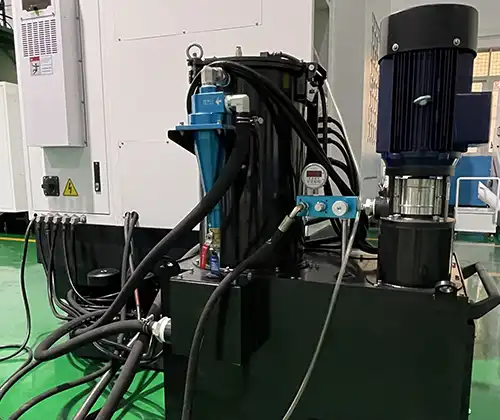
Internal Stress Releases; Bed Warps in 6 Months
Budget machine assemblers cut corners by using low-grade HT200 gray iron with single natural outdoor aging. After 6 to 12 months of heavy milling, trapped residual casting stresses relieve themselves, causing irreversible bed distortion and catastrophic loss of geometric alignment.
Full Metallurgical Reports; ±0.005mm Locked for 10 Years
Poured from certified Yunnan HT300 high-density pearlite gray iron with dense honeycomb ribbing. Undergoes secondary high-temperature thermal stress relief in computerized electric annealing ovens, permanently locking in JIS B6338 ±0.005mm precision.
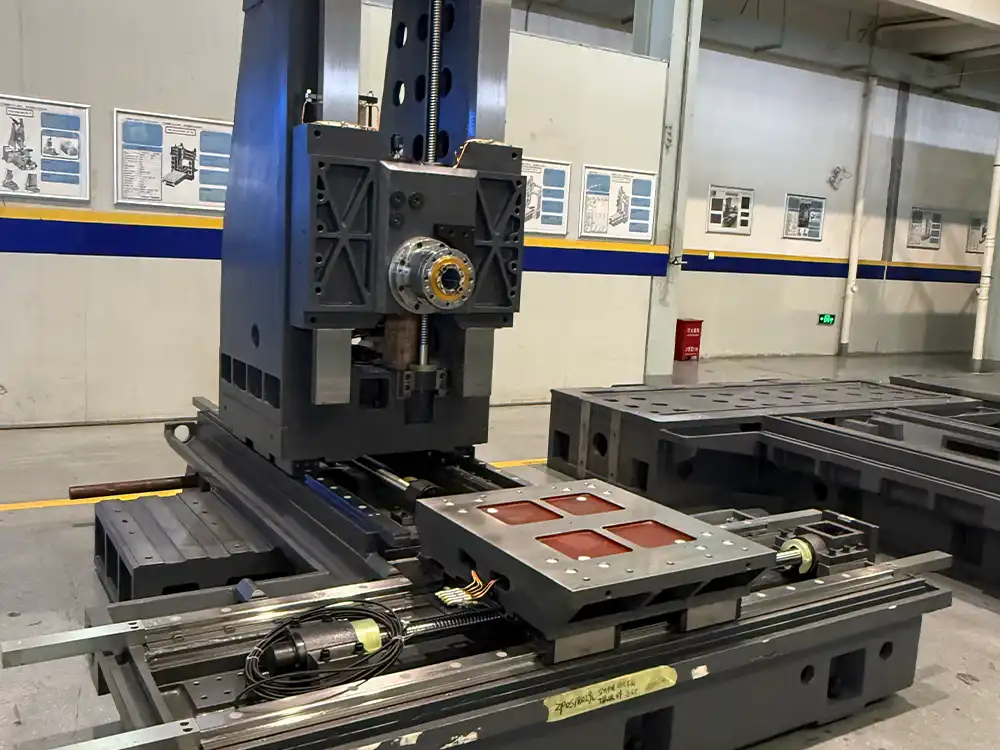
Certified Quality Inspection Reports & Engineering Downloads
Download genuine factory metallurgical quality certifications, electric oven secondary tempering records, and engineering catalog sheets.
Casting Secondary Tempering & Thermal Stress-Relief Report
Official 14-page electric oven heat-treatment tempering records verifying secondary stress-relief curves, eliminating residual internal stresses for permanent geometric precision.
Download Report (PDF)HT300 Gray Iron Structural & Metallurgical Inspection Report
Certified factory metallurgical and physical testing report confirming high-density pearlite HT300 gray iron castings, dense honeycomb ribbing, and zero internal casting porosity.
Download Report (PDF)German IF Precision Ballscrew Inspection & Quality Certificate
Official precision quality certificate for the German imported brand (IF) C3-ground ballscrew assembly, confirming micro-pitch accuracy and zero backlash motion.
Download Report (PDF)XDM-V540 Official Technical Specifications & Dimensional Drawings
Official machine dimensional footprint drawing, worktable T-slot schema, spindle torque curves, and electrical hookup specifications extracted from the factory manual.
Download Specs (PDF)Complete Technical Parameters (XDM-V540)
Fully tested and certified against Japanese Industrial Standard JIS B6338.
Travel & Working Envelope
| X/Y/Z-Axis Travel | 500 / 400 / 400 mm |
| Spindle Nose to Table | 100 - 500 mm |
| Spindle Center to Column | 430 mm (Short Throat) |
| Worktable Size (L × W) | 750 × 400 mm |
| Max Table Load Capacity | 300 kg |
| T-Slot Specifications | 3 - 18 × 126 mm |
Heavy-Duty BT40 Spindle System
| Spindle Taper & Interface | BT40 (7/24 Taper) |
| Max Spindle Speed | 8,000 rpm (Belt Drive) |
| Main Spindle Motor Power | 11 / 7.5 kW (Peak/Cont.) |
| Max Spindle Torque | 70 N·m (Continuous) |
| Center Coolant System (CTS) | 30 Bar (High-Pressure) |
| Max Solid U-Drill Diameter | Ø60 mm (304 Stainless) |
Motion, Feeds & Accuracy
| X/Y Rapid Traverse Rate | 36 m/min (#35 Roller Guides) |
| Z Rapid Traverse Rate | 24 m/min (Hardened Box Way) |
| Cutting Feedrate Range | 1 - 10,000 mm/min |
| Positioning Accuracy (JIS B6338) | ±0.005 mm |
| Repeatability (JIS B6338) | ±0.003 mm |
| Ball Screws Specification | Taiwan C3 Pre-Tensioned Ground |
Structure, Coolant & Utilities
| Cast Iron Material & Grade | Yunnan HT300 Pearlite Gray Iron |
| Heat Treatment Standard | 2× Electric Oven Annealing |
| Tool Magazine Capacity | 16T Twin-Arm Cam ATC |
| Machine Weight (Net / Gross) | 3,000 / 3,200 kg |
| Footprint Dimensions (L × W × H) | 1.63 × 1.80 × 2.45 m |
| Freight Elevator Compatibility | Compatible with 3,000 kg Lifts |
Request Official Machine Quote & Workpiece Evaluation
Share your material, hole specs, and monthly target volume. Our Chief Applications Engineer will evaluate cycle time feasibility and provide a detailed quotation within 24 hours.
- Complete machine layout drawings (CAD & 3D STEP).
- Free workpiece cycle time & tooling feasibility evaluation.
- Tiered export pricing with no hidden option markups.
- Direct 1-on-1 technical chat via WhatsApp.