1. Industry Overview & Structural Tube Challenges
Square steel tubing (e.g., Q235, Q345, AISI 1020, and 304 Stainless Steel) is a foundational structural material across furniture frames, retail display racks, and commercial fitness equipment. Offering high torsional strength and a clean aesthetic profile, square tubes are critical to modern modular design.
However, conventional multi-step fabrication workflows introduce significant operational bottlenecks:
- Process Fragmentation: Multi-machine transfers between standalone drilling rigs, manual tapping stations, and milling machines elevate handling risks and cumulative positional errors.
- Inadequate Thread Depth: Thin-walled square tubes (1.2 mm to 3.0 mm wall thickness) lack sufficient engagement threads, historically requiring costly secondary operations like weld nuts or blind rivet nuts (rivnuts).
- Dimensional Inconsistency: Manual positioning and tool changes often exceed acceptable engineering tolerances (failing ISO 2768-m standard limits).
- High Operating Costs: Excessive labor dependency and extended cycle times degrade profit margins in high-volume production.
2. Market Demand for Integrated CNC Tube Processing Solutions
As Industry 4.0 automation adoption accelerates, manufacturers require single-setup, multi-function CNC systems capable of performing thermal drilling, thread tapping, and contour milling on square and rectangular profiles.
Key Manufacturing Specifications
| Parameter | Standard Requirements | Integrated Drilling Solution |
|---|---|---|
| Machining Accuracy | ISO 2768-m (±0.1 mm) | High-precision servo control (±0.03 mm) |
| Thread Depth Ratio | 1.0× Nominal Diameter | 3.0× Nominal Diameter (via Thermal Form Bushing) |
| Cycle Time per Hole | 18–30 seconds (Multi-machine) | 3–6 seconds (Single-setup thermal drill + tap) |
| Material Thickness | 1.0 mm – 6.0 mm | 1.0 mm – 8.0 mm (Mild Steel, Stainless Steel, Aluminum) |
3. Technical Architecture of the Integrated Drilling Solution
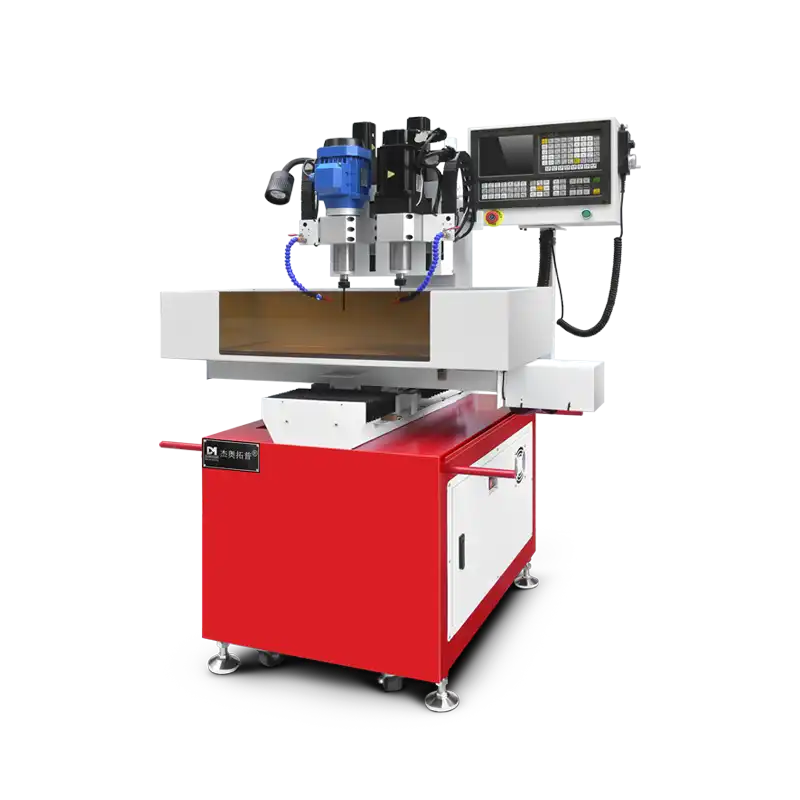
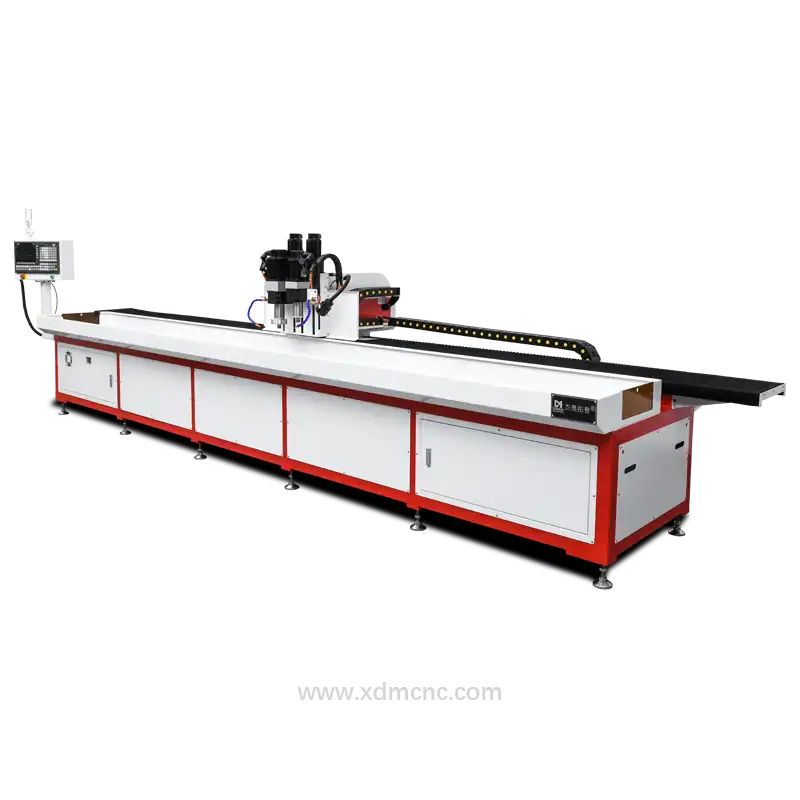
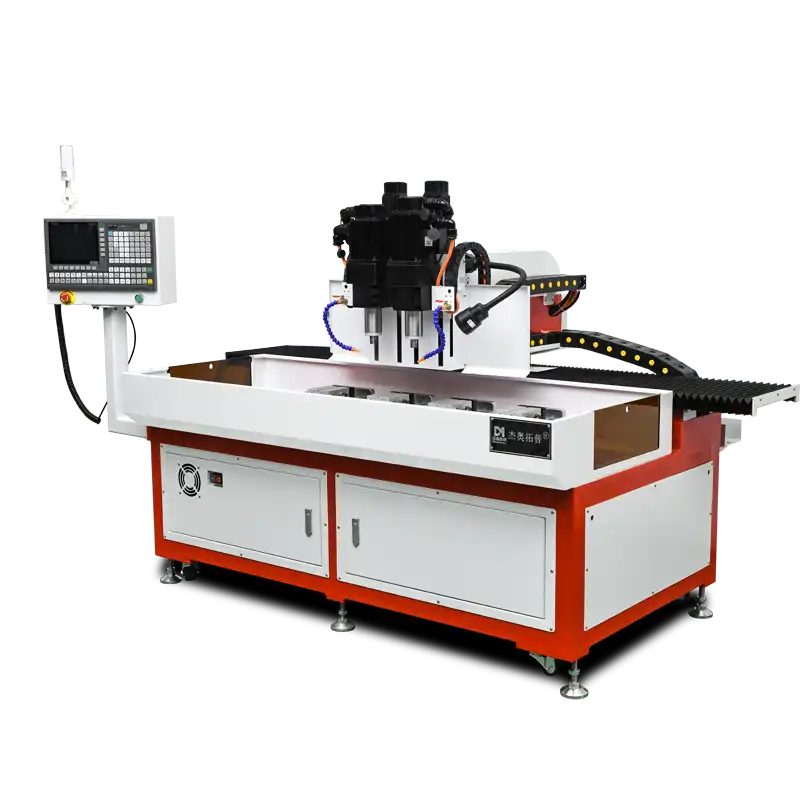
The DUOMI CNC Integrated Drilling Solution combines friction-thermal drilling technology with cold-forming tapping and multi-axis CNC positioning.
3.1 Core Subsystems
- High-Speed Thermal Drilling Head: Utilizes tungsten carbide friction drills operating at 2,000–4,000 RPM. Super-heated friction (~600°C–700°C) plasticizes structural steel locally, forming a downward collapsed collar that increases localized wall thickness by up to 300%.
- Synchronized Cold Forming Tapping Spindle: Applies roll taps (thread forming) compliant with DIN 13 / ISO 965 standards, creating chipless, work-hardened internal threads with up to 50% higher pull-out strength than cut threads.
- Automatic Tool Changer (ATC) & Magazine: Enables sub-2-second tool transitions between thermal drills, taps, and carbide end mills for localized slotting or clearance milling.
- Multi-Axis CNC Motion Controller: Features industrial touch-screen programming, G-code CAD/CAM integration, and automatic workpiece height sensing to account for tube wall bowing or mill tolerances.
3.2 Integrated Workflow Sequence
- Step 1: Workpiece loading & automated pneumatic/hydraulic clamping.
- Step 2: High-speed thermal drilling creates extruded bushing collar in parent metal.
- Step 3: Automatic tool change to cold-forming tap spindle.
- Step 4: Thread forming operation completed in seconds without chips.
- Step 5: Optional feature milling / slotting performed in same coordinate system.
- Step 6: Unclamping and automated part index/ejection.
4. Operational Advantages and Performance Benchmarks
4.1 Enhanced Thread Strength Without Fasteners
By forming a bush collar out of parent metal, the integrated drilling solution eliminates secondary hardware (weld nuts, clinch studs), cutting fastener material costs to zero while producing M4–M12 threads that easily withstand high dynamic forces in commercial fitness gear.
4.2 Floor Space & Labor Optimization
Replacing three independent machines (drill press, tapping unit, milling machine) with a single integrated unit reduces floor footprint by up to 60% and lowers direct labor requirement from 3 operators to 1 supervisor.
5. Industrial Application Case Studies
5.1 Modular Office Furniture Manufacturing
- Material: 30 × 30 mm square steel tube (1.5 mm wall thickness).
- Result: Transitioned from blind rivet nuts to thermal flow-drilled M6 threads. Reduced unit manufacturing cycle time by 35% and direct labor costs by 42%.
5.2 Heavy-Duty Retail Display Racks
- Material: 40 × 40 mm Q235 steel profiles with high pitch density drilling.
- Result: Positional accuracy reached ±0.04 mm across 2.5-meter long profiles, reducing structural misalignment rejection rates from 8.5% down to 0.3%.
5.3 Commercial Fitness Equipment Frames
- Material: 50 × 100 mm rectangular structural steel tubing (3.0 mm wall thickness).
- Result: Dynamic pull-out force tests confirmed thread retention exceeded 18.5 kN. Equipment structural durability ratings improved significantly while achieving 14-month total machine payback.
6. Financial Analysis & ROI Framework
| Expense / Metric | Traditional Process | Integrated Drilling Solution |
|---|---|---|
| Rivet Nut / Fastener Cost (100k holes) | $8,500 / year | $0 |
| Direct Labor (3 Operators vs 1) | $120,000 / year | $40,000 / year |
| Secondary Scrap Rate | 3.5% | < 0.5% |
| Estimated Payback Period | N/A | 11.4 Months |
7. Implementation Guidelines & Integration
- Workpiece Preparation: Ensure raw square tubing conforms to standard outer dimension tolerances (EN 10219 / ASTM A500).
- Tooling Selection: Choose specialized tungsten carbide friction bits tailored to workpiece material (mild steel vs stainless steel).
- Software Configuration: Utilize pre-loaded parametric program templates for rapid switching between variable hole pitch layouts.
Need High-Efficiency CNC Drilling & Tapping Machinery?
Consult with our senior application engineers to get a custom cycle time simulation and tailored machine proposal within 24 hours.