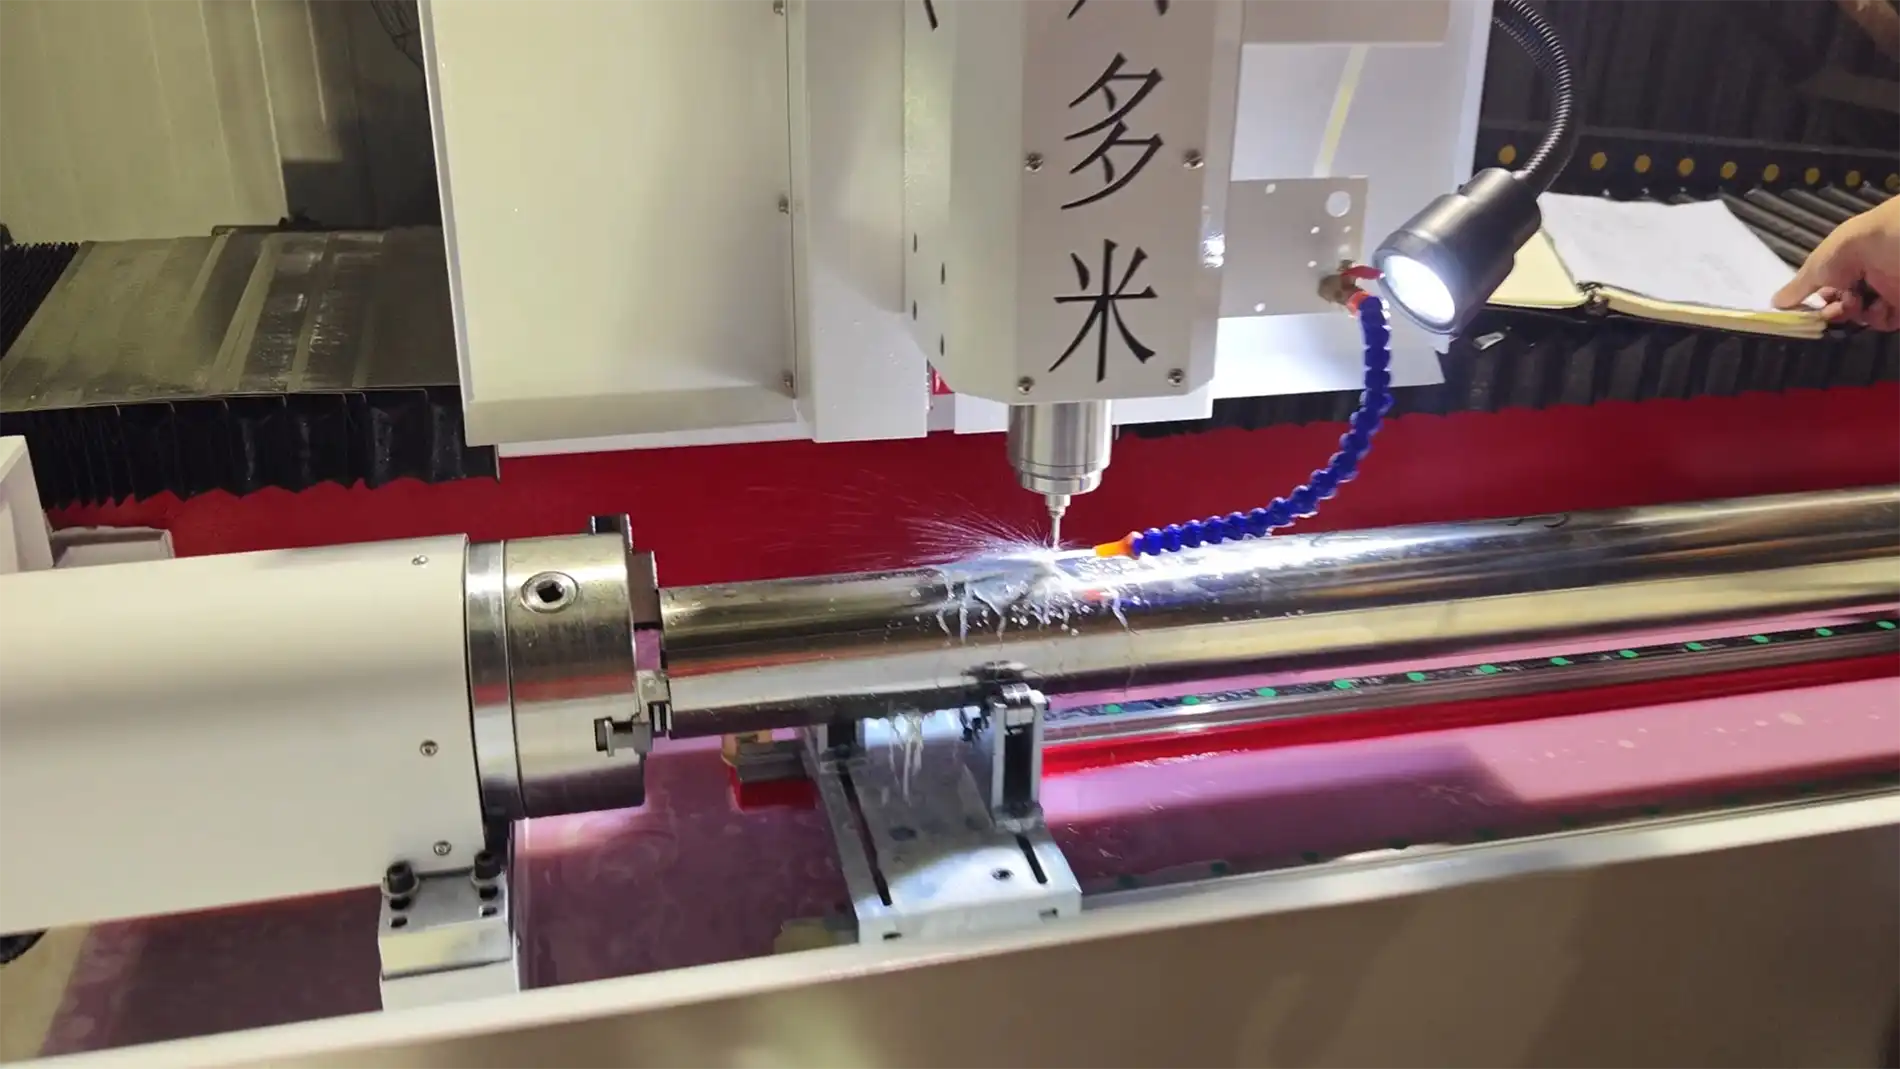
60,000 RPM Precision Micro-Drilling for 3-Meter Stainless Steel Food Mixing Tubes
Engineered for deep Ø0.8mm micro-orifices across 3.5mm-thick sanitary stainless steel pipes in food and pharmaceutical mixing equipment. Replaces manual bench drills with a 60,000 RPM motorized spindle and 360° A-axis CNC automation, eliminating 100% of deburring rework and preventing micro-tool breakage.
The 5-Step Continuous 3-Meter Pipe Micro-Drilling Process
How the DUOMI DNC-3003HD(R1) combines a 3000mm longitudinal stroke, 360° A-axis rotary indexing, and a 60,000 RPM motorized spindle to deliver burr-free sanitary orifices in stainless steel tubes.
3-Meter Tube Loading & Concentric Alignment
The operator loads the stainless steel tube (up to 3000mm long) into the heavy-duty A-axis rotary chuck, with intermediate bed supports and pneumatic tailstock clamping the opposing end.
Parametric Matrix Setup & Coordinate Verification
The operator calls the programmed hole matrix containing axial pitch spacing (X-axis) and circumferential radial angles (A-axis). The Z-axis datum offsets verify automatically.
High-Speed Radial Micro-Feed Penetration
The motorized micro-spindle accelerates to 60,000 RPM. Driven by rigid ball screws and hand-scraped ways, the solid carbide Ø0.8mm micro-drill engages the cylindrical outer wall perpendicular to the tube axis.
High-Velocity Breakthrough & Chip Evacuation
At 60,000 RPM, the tool achieves true high-speed shear velocity, penetrating the 3.5mm wall (4.4:1 aspect ratio) while evacuating micro-chips cleanly.
Continuous Multi-Orifice Indexing & Unloading
The Z-axis retracts, the X-axis traverses, and the A-axis indexes to the next angular coordinate without stopping, running hundreds of orifices autonomously until the tube finishes.
Throughout the cycle, the rigid hand-scraped bed, 3000mm X-axis, and 60,000 RPM micro-spindle operate seamlessly, turning complex deep micro-drilling on long tubes into an autonomous precision cell.
Operational Transformation: Precision Micro-Drilling in 3-Meter Stainless Steel Food Mixing Tubes
Customer: Jiangsu Yixin Pharmaceutical Equipment Co., Ltd.
Part: Sanitary Stainless Steel Mixing Shaft Tubes (Ø0.8mm micro-holes through 3.5mm wall depth, up to 3000mm length, 304/316L austenitic stainless steel)
Legacy Process: Manual Bench Drills + High Tool Breakage + Hand Deburring
The equipment manufacturer previously relied on manual bench drills to produce deep Ø0.8mm orifices in thick-walled (3.5mm) stainless steel tubes. Under manual feed, fluctuating operator thrust caused severe tool buckling, thermal binding, and frequent drill bit breakage at the 4.4:1 depth-to-diameter ratio. Slanted contact against the outer cylinder wall induced tool walk-off, causing off-center holes and egg-shaped entries. Breakthrough tears created massive internal exit burrs that trapped food particles and violated sanitary Clean-in-Place (CIP) standards. Workers spent extensive hours manually scraping and deburring each orifice under magnification, which scratched sanitary surfaces, drove up scrap rates, and tied down multiple skilled workers.
DUOMI Solution: DNC-3003HD(R1) Long-Bed Pipe CNC Micro-Drilling Center
Dedicated DUOMI DNC-3003HD(R1) 4-Axis Long-Bed CNC Pipe Drilling Machine featuring a 3000mm X-axis stroke, 360° continuous A-axis rotary chuck (Ø10mm–Ø200mm tube capacity), hand-scraped base guideways, pneumatic tailstock with intermediate steady rests, and a 60,000 RPM motorized high-frequency micro-spindle.

Verified Operational Comparison: Legacy Manual Bench Drill vs. DUOMI DNC-3003HD(R1)
| Metric | Legacy Manual Bench Drill | DUOMI DNC-3003HD(R1) CNC Center |
|---|---|---|
| Spindle Speed & Cutting Mode | Low RPM manual press; prone to rubbing & work-hardening | 60,000 RPM motorized spindle; pure high-velocity shearing |
| Micro-Tool Breakage & Wear | Frequent drill buckling and breakage from manual feed variance | Controlled tool wear; drill breakage eliminated via CNC micro-feed |
| Long-Pipe Workpiece Capacity | Segmented re-clamping required for tubes exceeding 1 meter | Continuous 3000mm travel envelope in a single rigid setup |
| Radial Indexing & Positioning | Manual line scribing with cumulative positional drift | 360° continuous A-axis CNC rotary chuck with ±0.02mm repeatability |
| Exit Hole Quality & Burrs | Heavy inner wall plastic tearing & rollover burrs | Clean burr-free orifice edges; 100% compliant with sanitary CIP |
| Secondary Deburring Labor | Hours of manual scraping under magnification per tube | Zero manual deburring required; direct flow to final assembly |
| Hole Geometry & Roundness | Tool walk-off produced egg-shaped entries and off-center holes | Rigid radial entry guarantees perfect roundness and symmetry |
| Operator Labor Allocation | 1 dedicated operator per manual press; high physical fatigue | 1 operator oversees multiple CNC machines running continuously |
Customer ROI: More Output. Fewer Operations. Lower Cost per Part. By replacing manual bench drills with the DUOMI DNC-3003HD(R1), Jiangsu Yixin Pharmaceutical Equipment eliminated 100% of manual deburring labor, brought micro-drill bit breakage under control, achieved ±0.02mm hole repeatability along 3-meter tubes, and enabled a single operator to manage multiple automated CNC drilling centers simultaneously.
Data reflects verified production metrics from pharmaceutical and food machinery component manufacturing. Actual cycle times and tool longevity depend on stainless steel alloy grade, wall thickness, hole diameter, and hole array density.
Engineered Specifically for Long Stainless Pipe Micro-Orifice Drilling
Conventional vertical machining centers cannot support 3-meter pipe lengths, while standard drills lack the 60,000 RPM velocity required for burr-free micro-holes in work-hardening stainless steel.
60,000 RPM High-Frequency Micro-Spindle
Provides the ultra-high peripheral cutting speed needed to shear ductile stainless steel cleanly, preventing work-hardening, built-up edge, and tool tip buckling.
3000mm Long-Stroke Rigid Bed
Continuous 3-meter X-axis travel with pneumatic tailstock and intermediate steady rests accommodates long sanitary mixing pipes in a single setup.
360° Continuous A-Axis Rotary Chuck
Precision CNC rotary indexing unit clamps tubes from Ø10mm to Ø200mm, executing dense circumferential hole patterns with zero manual re-clamping.
Hand-Scraped Ways & Vibration Damping
Base guideway mating surfaces are hand-scraped (1–3 µm relief) to eliminate residual stress and dampen high-frequency harmonics at 60,000 RPM.
±0.02mm API Laser Verified Accuracy
100% factory pitch-compensated via API laser interferometer, guaranteeing hole pitch consistency across the entire 3000mm span.
1-Operator Multi-Machine Productivity
Autonomous canned micro-drilling routines free operators from physical feeding, allowing one technician to oversee multiple CNC units.
Frequently Asked Questions
Engineering, sanitary compliance, and operational clarity for food and pharmaceutical equipment manufacturers.
Why does manual drilling cause excessive tool breakage in thick-wall stainless steel tubes?
A Ø0.8mm micro-drill has virtually no bending stiffness. When drilling a 3.5mm wall (4.4:1 aspect ratio), manual thrust forces fluctuate constantly, triggering buckling instability. Simultaneously, austenitic stainless steel work-hardens upon rubbing, creating excessive localized heat that binds micro-chips inside the flutes. At 60,000 RPM, the tool achieves high cutting speed with steady, programmable feed rates, cutting by pure shear and preventing tool breakage.
How does the machine eliminate inner exit burrs without requiring secondary deburring?
Under low cutting speeds, ductile stainless steel tears and extrudes outward as the drill breaks through the inner tube wall, creating heavy rollover burrs. The DUOMI DNC-3003HD(R1) runs at 60,000 RPM, delivering the high surface velocity required to cleanly shear chips at the exit boundary. This leaves pristine inner edges directly off the machine, eliminating 100% of secondary deburring.
Why is inner hole burr-free quality so critical for food mixing equipment?
In sanitary food and pharmaceutical mixing equipment, inner-wall burrs create crevices where product residues accumulate, fostering bacterial growth and obstructing Clean-in-Place (CIP) sterilization. Furthermore, loose burrs can detach into mixing batches, causing severe contamination. Burr-free orifices guarantee full sanitary compliance and smooth fluid flow.
How does the machine support 3-meter long tubes without sag or vibration?
The DNC-3003HD(R1) features a dedicated 3000mm longitudinal bed equipped with an A-axis rotary chuck, a pneumatic tailstock, and adjustable intermediate steady rests. Combined with hand-scraped guideways that absorb cutting vibrations, the system maintains concentricity and stability across the entire 3-meter length.
How does this platform enable a single operator to run multiple machines?
Unlike manual bench drilling where an operator must feed every single hole by hand, the DUOMI DNC-3003HD(R1) operates fully automatically. Once the operator loads the 3-meter tube and presses Cycle Start, the machine executes the complete longitudinal and radial hole array autonomously, freeing the technician to manage adjacent machines.
DNC-3003HD(R1) Long-Bed Pipe CNC Micro-Drilling Machine — Specifications
Click to Expand Full Technical Specifications (15)
| Machine Model | DNC-3003HD(R1) |
| Machine Type | Specialized 4-Axis Long-Bed Pipe CNC Micro-Drilling Machine |
| X-Axis Machining Stroke | 3000 mm (Precision Ball Screw & Linear Guideways) |
| Z-Axis Micro-Feed Stroke | 200 mm |
| Rotary A-Axis Indexing | 360° Continuous Rotational Indexing Unit |
| Tube Clamping Diameter | Ø10 mm – Ø200 mm |
| Max Workpiece Length | Up to 3000 mm (Accommodates 3-Meter Long Pipes) |
| Spindle Type | High-Frequency Motorized Electric Micro-Spindle |
| Spindle Speed | 0 – 60,000 RPM (Stepless High-Frequency Inverter Control) |
| Drilling Diameter Range | Ø0.3 mm – Ø3.0 mm (Micro-Drill Dedicated Collet) |
| Machine Bed Construction | Hand-Scraped Heavy Cast Iron Bed (1–3 µm Planar Relief) |
| Positioning Repeatability | ±0.02 mm (API Laser Interferometer Compensated) |
| Tailstock & Support | Pneumatic Tailstock + Intermediate Adjustable Steady Rests |
| Operating Mode | Automated Non-Stop Continuous G-Code Cycle |
| Safety & Quality Standard | CE Certified Machinery Directive, Fully Guarded Metal Enclosure |
Request a Free Sample Machining & Feasibility Analysis
Send your tube dimensions, material grade, and thread specifications. Our tooling engineers will verify feasibility, calculate cycle time, and run a live machining test on your spec.