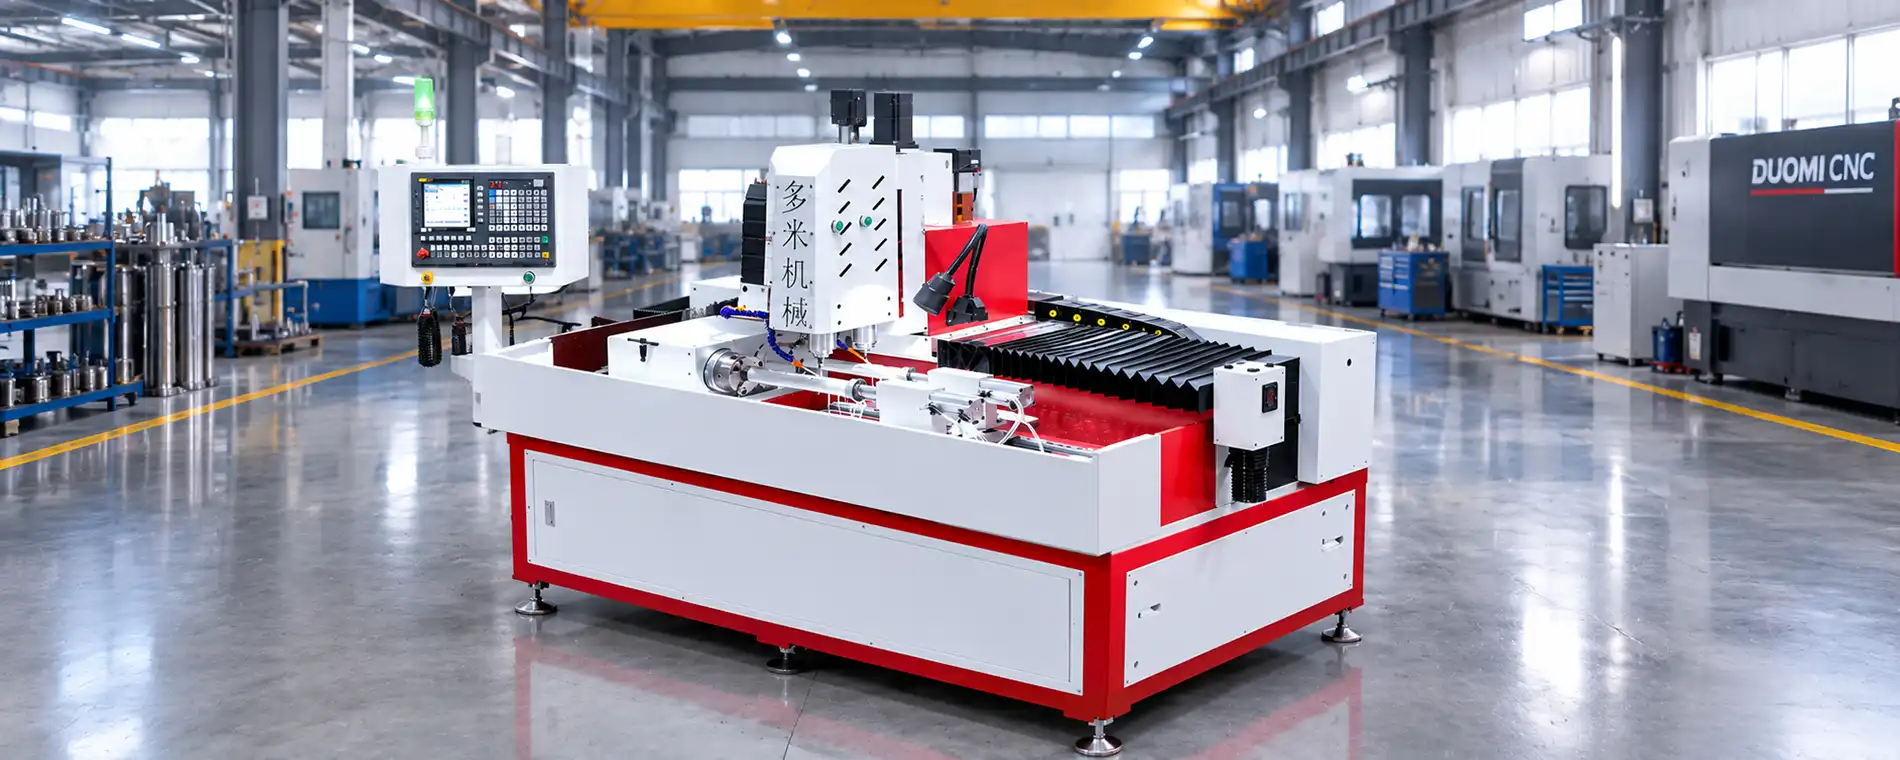
Synchronous Dual-Spindle Micro-Drilling for Round Aluminum Heat Dissipation & Acoustic Tubes
Engineered for Φ1.0mm acoustic and thermal ventilation hole arrays through 2.0mm round aluminum tubing in consumer electronics. Twin 60,000 RPM motorized spindles and dual synchronized 360° rotary chucks double batch output while eliminating 100% of manual deburring.
The 5-Step Dual-Spindle High-Speed Micro-Drilling Process
How the DUOMI DNC-500DD(R2) synchronizes twin 60,000 RPM electric spindles and dual 360° rotary chucks to deliver burr-free micro-holes on round aluminum tubes in a single continuous cycle.
Simultaneous Workpiece Loading & Concentric Clamping
The operator mounts two raw aluminum tubes (up to Ø70mm) into the dual synchronized pneumatic rotary chucks. Controlled radial clamping force grips thin-walled profiles firmly without out-of-round distortion.
Digital Coordinate Setup & Job Selection
The operator calls up the target hole matrix program from the 10,000-program memory bank. Dual Z-axis tool offsets and rotary reference angles align automatically with zero manual punch scribing.
Ultra-High-Speed Burr-Free Penetration
Twin 2.2kW direct-drive spindles ramp instantly to 60,000 RPM. Entering the convex cylindrical wall at extreme linear peripheral velocity, the solid carbide micro-drills cut by pure shearing rather than thermal tearing.
Synchronized Micro-Pecking & Dual 360° Indexing
CNC canned micro-peck routines pierce the 2.0mm wall depth (2:1 aspect ratio), expelling chips cleanly before heat concentrates. Synchronously, dual 360° A-axes index both tubes to each circumferential angle in locked harmony.
Finished Burr-Free Unloading & Direct Assembly
Both finished tubes are unloaded with 100% verified hole counts, flawless internal exit bore cleanliness, and strict hole pitch symmetry. Parts move directly to anodizing or acoustic assembly without secondary deburring.
Throughout the cycle, the dual 60,000 RPM spindles and synchronized rotary drives operate in parallel harmony, doubling throughput while turning precision tube micro-drilling into a single-operator automated cell.
Operational Transformation: Synchronous Dual-Spindle Micro-Drilling for Round Aluminum Tubing
Customer: Huizhou Qiqi Pulian'ai Hardware Products Co., Ltd.
Part: Round Aluminum Tubing for Acoustic Speaker Meshes & Hair Dryer Thermal Dissipation Tubes (Φ1.0mm holes through 2.0mm wall thickness, Ø70mm max tube diameter).
Legacy Process: Single-Spindle Drilling + Low Cutting Velocity + Manual Bench Deburring
The manufacturer previously relied on conventional single-spindle drilling setups running at low-to-medium rotational speeds to produce micro-ventilation holes on soft aluminum tubes. At standard cutting speeds, the ductile aluminum tore and deformed rather than cutting cleanly, resulting in stubborn rollover burrs at the inner exit holes and heavy built-up edge on micro-drill tips. Drilling on the cylindrical tube surface frequently caused drill deflection and tool breakage at the 2:1 depth-to-diameter ratio. Every single part required secondary manual deburring under magnification by dedicated fitters with micro-scrapers, which introduced surface scratches on cosmetic exterior tubes, caused high scrap rates, and created a severe capacity bottleneck during volume delivery.
DUOMI Solution: DNC-500DD(R2) Dual-Spindle High-Speed CNC Micro-Drilling Machine
Dedicated DUOMI DNC-500DD(R2) 4-Axis CNC Micro-Drilling Machine equipped with twin 2.2kW 60,000 RPM high-speed motorized electric spindles, dual synchronized 360° continuous rotary workholders (≤Ø70mm clamping capacity), an 800kg vibration-dampened cast structure, and high-precision guideways (parallelism ≤0.01mm/1000mm).
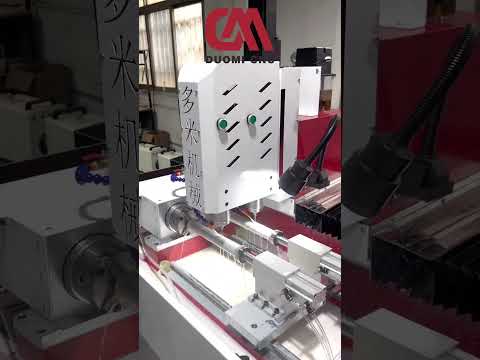
Verified Operational Comparison: Legacy Single-Spindle vs. DUOMI DNC-500DD(R2)
| Metric | Legacy Single Spindle + Hand Deburring | DUOMI DNC-500DD(R2) Dual Spindle |
|---|---|---|
| Spindle Configuration & Speed | Single spindle at low-to-medium RPM; prone to material tearing | Twin 2.2kW motorized spindles running at 0 – 60,000 RPM |
| Workpiece Processing Capacity | Single tube clamping; 1 part drilled per machine cycle | Dual synchronized 360° rotary chucks (≤Ø70mm × 2 parts in parallel) |
| Cycle Throughput & Output | Baseline single-unit production capacity | +100% throughput expansion (doubled finished parts per cycle) |
| Hole Quality & Exit Burrs | Heavy inner wall exit burrs & built-up edge (BUE) on drill flutes | Burr-free clean shear across Φ1.0mm holes × 2.0mm wall depth |
| Post-Machining Secondary Labor | 100% manual deburring under magnification; scratch risk on finish | Zero manual deburring required; direct flow to anodizing/assembly |
| Positioning & Pitch Consistency | Subject to manual clamping drift and uneven hole pitch | ≤0.02mm positioning accuracy & repeat positioning fidelity |
| Machine Operator Allocation | High labor intensity; 1 operator per machine plus deburring fitters | 1 operator manages automated cell with zero secondary finishing |
| Setup Agility & Storage | Time-consuming manual setup adjustments for different hole matrices | Approx. 10,000 programs memory; instant switching from R&D to mass runs |
Customer ROI: More Output. Fewer Operations. Lower Cost per Part. By upgrading to the DUOMI DNC-500DD(R2) dual-spindle micro-drilling platform, Huizhou Qiqi Pulian'ai Hardware doubled finished unit throughput (+100%), eliminated manual deburring labor entirely, protected exterior aluminum finishes from scratch damage, and achieved agile switching between fast new product prototyping and volume order delivery.
Data reflects verified production metrics from hardware and acoustic component manufacturing. Actual cycle times and tool longevity vary with tube wall thickness, alloy temper, hole matrix density, and micro-drill geometry.
Engineered Specifically for High-Speed Precision Micro-Drilling on Round Tubing
Standard vertical machining centers and generic drill presses lack the rotational velocity and synchronized dual workholding needed for thin-walled round tubes. The DNC-500DD(R2) combines 60,000 RPM cutting velocity with twin-axis productivity.
Twin 60,000 RPM High-Speed Motorized Spindles
Two independent 2.2kW electric spindles achieve up to 60,000 RPM, providing the high peripheral shear velocity needed to drill ductile aluminum cleanly without plastic tearing or exit burrs.
Synchronized Dual 360° Rotary Stations
Two dedicated rotary workholders (≤Ø70mm capacity) index simultaneously in locked angular harmony, enabling parallel two-tube drilling across the 500mm X-axis stroke.
Burr-Free Micro-Hole Surface Integrity
High cutting speeds transition aluminum cutting into pure shear mode, eliminating built-up edge on carbide micro-drills and leaving bore walls and exits perfectly crisp.
Sub-0.02mm High-Precision Motion Mechanics
Rigid cast frame (~800kg) with guideway parallelism ≤0.01mm/1000mm and positioning accuracy ≤0.02mm eliminates dynamic vibration at 60,000 RPM.
Dual Programming & 10,000-Program Memory
Integrates CAM computer G-code programming with direct manual conversational CNC input, backed by ~10,000 job files storage for seamless product changeovers.
Single-Operator Cell & Total Deburring Elimination
Fully automated dual-part cycle frees operators to oversee adjacent cells while removing 100% of manual secondary deburring and scraping operations.
Frequently Asked Questions
Practical engineering, quality, and operational clarity for hardware and electronics OEMs.
Why do standard drilling speeds cause severe exit burrs and material tearing in aluminum tubing?
Aluminum is a soft, ductile alloy with high thermal conductivity and a low melting point. At standard drilling speeds, the peripheral cutting velocity is too low to produce crisp shear fracture. Instead, the tool pushes and plastically deforms the metal, creating heavy built-up edge (BUE) on the drill and extruded rollover burrs as it exits the inner tube wall. Running at 60,000 RPM provides the ultra-high surface velocity required to shear chips instantly before thermal deformation occurs.
How does the dual-spindle architecture double throughput without requiring two operators?
The DNC-500DD(R2) features twin 2.2kW spindles paired with dual synchronized 360° rotary fixtures on a single rigid 800kg bed. Both spindles drill two identical tubes simultaneously within a compact 1400×1600mm footprint. The operator loads both tubes in a single setup, selects the program, and initiates the automated cycle, effectively doubling production output with zero increase in labor headcount.
How does the machine prevent drill walking and bit breakage on cylindrical tube surfaces?
Drilling a Φ1.0mm micro-hole into a convex cylindrical surface introduces severe radial deflection forces. The DNC-500DD(R2) combines ultra-high spindle speed (60,000 RPM) with high-rigidity linear guideways (parallelism ≤0.01mm/1000mm) and automated canned micro-pecking cycles. The drill enters at high surface speed, cleanly engaging the material without surface skidding, while rapid micro-retracts clear chips from the 2:1 depth-to-diameter bore.
Can the DNC-500DD(R2) accommodate thin-walled tubes without clamping distortion?
Yes. The dual rotary stations feature precision chucks engineered specifically for thin-walled hollow profiles up to Ø70mm. The clamping pressure is uniformly distributed around the circumference to prevent ovality or out-of-round deformation while maintaining rigid grip against cutting forces during 360° indexing.
How flexible is the machine for switching between R&D prototyping and high-volume manufacturing?
The control system features an internal storage bank for approximately 10,000 programs and supports both CAM G-code file transfers and conversational manual on-screen programming. Operators can switch between different tube diameters, hole spacing patterns, or acoustic mesh layouts in minutes without re-tooling the mechanical chassis.
DNC-500DD(R2) Dual-Spindle High-Speed CNC Micro-Drilling Machine — Specifications
Click to Expand Full Technical Specifications (19)
| Machine Model | DNC-500DD(R2) |
| Machine Type | Dual-Spindle 4-Axis CNC High-Speed Micro-Drilling Machine |
| Machining Travel (X * Z * A) | X: 500 mm, Z: 200 mm, A: 360° Continuous Rotary |
| Rotary Clamping Capacity | ≤ Ø70 mm × 2 Synchronized Stations (Dual Workholders) |
| Spindle Configuration | Twin Motorized Electric High-Speed Spindles (2 Units) |
| Spindle Power | 2.2 kW × 2 Spindles (High-Torque Electric Motors) |
| Spindle Speed Range | 0 – 60,000 RPM × 2 (Stepless Frequency Inverter Control) |
| Drilling Diameter Range | Ø0.3 mm – Ø3.0 mm (Precision Micro-Hole Range) |
| Guideway Parallelism | ≤ 0.01 mm / 1000 mm |
| Guideway Flatness | ≤ 0.02 mm / 1000 mm |
| Positioning Accuracy | ≤ 0.02 mm |
| Repeated Positioning Accuracy | ≤ 0.02 mm / 1000 mm |
| Backlash (Pre-Compensation) | 0.02 mm |
| Operating Voltage | AC 220V (Single-Phase / Standard Industrial Grid) |
| Program Storage Capacity | Approx. 10,000 Programs Memory Bank |
| Programming Mode | Dual Mode: CAM / Computer Programming & Manual Shop-Floor Input |
| Machine Footprint & Dimensions | 1,400 × 1,600 × 1,700 mm (W × D × H) |
| Machine Weight | Approx. 800 kg (High-Rigidity Vibration-Dampened Cast Base) |
| Safety & Quality Standard | CE Certified Machinery Directive, Fully Guarded Metal Enclosure |
Request a Free Sample Machining & Feasibility Analysis
Send your tube dimensions, material grade, and thread specifications. Our tooling engineers will verify feasibility, calculate cycle time, and run a live machining test on your spec.