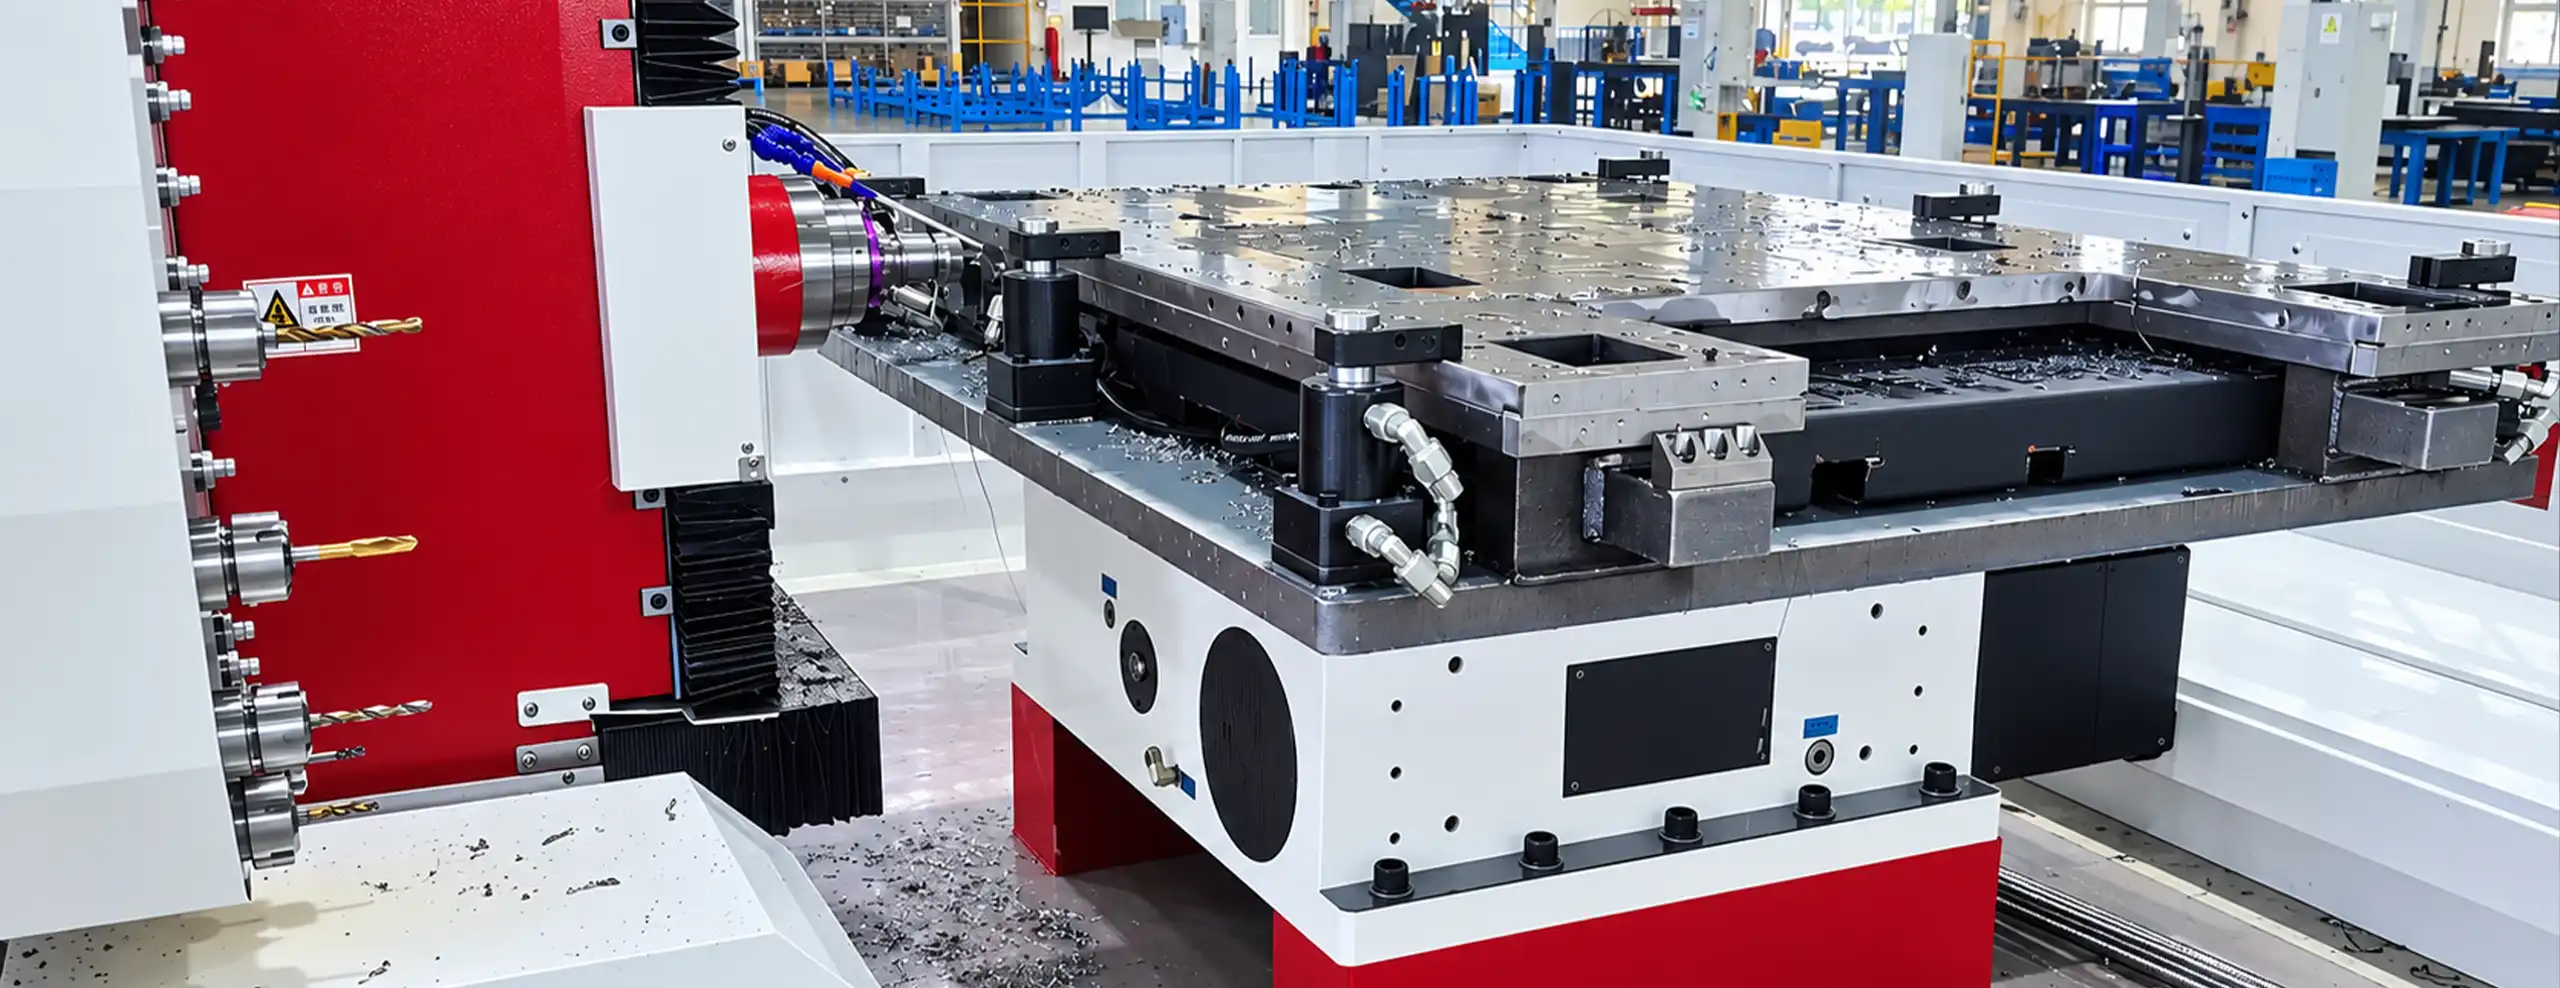
Consolidating 4-Sided Drilling, Slotting & Rigid Tapping for Large Welded Assemblies
Engineered for 1.4m × 0.8m welded structural steel plates in stage lift infrastructure. Replaces high-CAPEX gantry machines and error-prone offline manual tapping with single-setup 360° rotary automation, eliminating crane flips and stopping M5 tap breakage.
The 5-Step Consolidated 4-Axis Multi-Side Machining Process
How the DUOMI 1630N10(R1) integrates 360° A-axis indexing, high-torque BT30 rigid tapping, and traveling ATC to machine heavy welded plates in a single continuous setup.
Heavy Plate Loading & Datum Locking
The operator uses an overhead crane a single time to mount the 1.4m × 0.8m welded steel assembly onto the heavy-duty T-slot A-axis rotary fixture. The primary zero-point datum is probed and locked for all four lateral faces.
Automated 4-Sided Drilling & Slot Milling
The CNC program commands the cast iron A-axis table to index through 360°, presenting Faces 1 through 4 sequentially. The high-rigidity mechanical spindle performs spot drilling, deep-hole drilling, and interpolation milling for elongated slots and Φ8 dowel pin holes.
In-Line Tool Swaps via Traveling Servo Magazine
The 10-tool disc magazine moves directly with the traveling spindle carriage along the 1.6m X-axis, swapping drills, slot mills, and taps locally adjacent to the cutting zone in under 2 seconds.
Synchronized CNC Rigid Tapping (M5, M8, M10)
Without removing the workpiece from the machine, the BT30 spindle switches into encoder-synchronized rigid tapping mode, threading all M5, M8, and M10 holes directly on-machine to exact program depth.
Single-Crane Unloading & Direct Integration
Once all four perimeter faces are completely drilled, slotted, and tapped, the A-axis returns to home. The finished plate is unclamped and lifted off in a single crane cycle, fully ready for stage lift frame assembly.
Throughout the cycle, the precision A-axis rotary table, traveling 10-tool servo ATC, and high-torque mechanical spindle synchronize seamlessly, converting rough welded fabrications into finished precision platforms.
Operational Transformation: Consolidating 4-Sided Machining on 1.4m × 0.8m Welded Assemblies
Customer: Stage Lift & Heavy Mechanical Infrastructure Manufacturer
Part: Heavy Welded Structural Steel Plates (1.4m × 0.8m, perimeter M5/M8/M10 threaded holes, Φ8 dowel pin holes, elongated guide slots)
Legacy Process: Gantry Machine + Right-Angle Head + Offline Bench Tapping
The manufacturer previously relied on a high-CAPEX gantry milling machine fitted with an external right-angle side-milling head to drill perimeter holes on 1.4m × 0.8m welded steel plates. Because the gantry lacked automated part rotation, operators used overhead cranes to unclamp, lift, flip, and re-clamp the heavy workpiece 4 separate times, destroying the primary datum and causing cumulative alignment errors exceeding 0.08mm. The cantilever right-angle head suffered from severe chatter during slot milling, while the lack of on-machine tapping forced parts offline to fitters using handheld pneumatic tools. Frequent M5 tap breakage scrapped high-value welded assemblies, and crane operations tied up the costly gantry machine for hours with light side work.
DUOMI Solution: 1630N10(R1) Horizontal 4-Axis CNC Drilling & Tapping Machining Center
Dedicated DUOMI DNC-1630N10(R1) 4-Axis Horizontal CNC Drilling & Tapping Machine equipped with an integrated heavy-cast A-axis 360° rotary table, 1600mm × 300mm × 600mm machining stroke, 5.5kW Taiwan BT30 mechanical spindle with synchronized rigid tapping, a traveling 10-tool disc ATC moving with the spindle.
Verified Operational Comparison: Legacy Gantry Route vs. DUOMI 1630N10(R1)
| Metric | Legacy Gantry + Hand Tapping | DUOMI 1630N10(R1) Horizontal 4-Axis |
|---|---|---|
| Part Setups & Handling | 4 manual crane flips & re-clamping cycles per plate | 1 single clamping setup on 360° A-axis table (75% handling cut) |
| Datum Repeatability | Variable stack-up error (>0.08mm) from repeated manual flips | Stable ≤0.02mm positioning repeatability across all 4 faces |
| Threading Execution | Offline manual/pneumatic bench tapping by fitters | In-machine CNC synchronized rigid tapping (M3 to M18) |
| Tooling & Rigidity | Cantilever right-angle head attachment; prone to severe chatter | Direct-drive BT30 mechanical spindle (+50% tool life) |
| Defect & Scrap Risk | 3% to 5% scrap rate from broken M5 taps & missed threads | 0% scrap rate; automated G-code execution eliminates tap breakage |
| Total Cycle Time per Part | 45 minutes per plate (cutting + handling + bench tapping) | 26 minutes per plate (42% cycle time reduction) |
| Operator Safety (EHS) | Hazardous manual crane-assisted flipping of heavy weldments | Single load/unload cycle; fully enclosed protected workspace |
| Asset Utilization (CAPEX) | High-CAPEX gantry machine idling while waiting for crane flips | Freed gantry center for high-value heavy surface milling (>85% OEE) |
Customer ROI: More Output. Fewer Operations. Lower Cost per Part. By replacing gantry side-milling and manual bench tapping with the DUOMI 1630N10(R1), the manufacturer cut cycle time by 42%, eliminated 100% of tap breakage scrap, and freed multi-million-dollar gantry machinery for high-margin heavy milling. Following two continuous months of zero-defect production, the customer issued a formal repeat purchase order to expand cell capacity.
Operational data verified in continuous production by stage lift equipment manufacturer. Actual cycle times vary depending on plate dimensions, weldment hardness, hole matrix density, and thread specifications.
Engineered Specifically for Heavy Plate Multi-Face Machining
Standard vertical machining centers and large gantry mills cannot efficiently handle multi-surface perimeter drilling, slotting, and tapping on heavy weldments. The 1630N10(R1) integrates 1.6m horizontal reach with 360° rotary turnover.
Integrated Cast Iron 360° A-Axis Table
Heavy-duty continuous rotary platform rotates 1.4m × 0.8m welded plates smoothly to all four lateral faces, eliminating crane flips and preserving the master coordinate datum.
High-Torque BT30 Mechanical Spindle
5.5kW Taiwan mechanical spindle provides high dynamic rigidity and sustained torque for deep-hole drilling, slot milling, and in-machine rigid tapping from M3 to M18.
Spindle-Mounted Traveling Disc ATC
10-tool servo disc magazine travels directly alongside the spindle carriage across the 1.6m X-axis, swapping tools in under 2 seconds adjacent to the cutting zone.
1600mm Long-Stroke Horizontal Structure
Generous travel envelope of X: 1600mm, Y: 300mm, and Z: 600mm completely encompasses large stage lift plates, structural frames, and heavy sheet fabrications.
API Laser Calibrated Precision (≤0.02mm)
100% factory inspected and pitch-error compensated with US-imported API laser interferometers, ensuring hole pitch, dowel pin centers, and slot coordinates stay within ≤0.02mm.
CAPEX Optimization & Gantry Relief
Right-sizes lateral drilling and tapping into a compact, dedicated cell, liberating multi-million-dollar gantry machining centers to focus on high-margin heavy top milling.
Frequently Asked Questions
Practical engineering, quality, and operational clarity for structural steel and equipment OEMs.
Why is single-setup clamping so critical for heavy stage lift platforms?
Stage lift platforms feature tight dowel pin alignment holes (Φ8) and mounting hole patterns across all four perimeter sides. Flipping heavy 1.4m × 0.8m plates four separate times with overhead cranes introduces cumulative re-clamping errors exceeding 0.08mm, causing binding or jamming during onsite lift assembly. Clamping once on a 360° rotary table holds all side hole positions strictly within ≤0.02mm referenced to a single datum.
How does in-machine CNC rigid tapping eliminate M5 tap breakage compared to manual tapping?
Manual handheld pneumatic tapping depends entirely on operator arm stability, making it difficult to maintain a strict 90° angle against vertical plate edges. Small M5 taps easily bind, tilt, and break inside deep holes, ruining finished welded plates. The DUOMI BT30 mechanical spindle coordinates Z-axis feed and spindle rotation with servo encoder synchronization, ensuring perfect thread lead, zero tap breakage, and 100% thread depth consistency.
How does the 1630N10(R1) outperform an external right-angle milling head mounted on a gantry?
An external right-angle milling head attaches as a cantilever overhang accessory to a vertical gantry spindle, introducing excessive mechanical play, high chatter, and low cutting rigidity during heavy drilling or slot milling. Furthermore, auxiliary heads cannot tap threads or change tools automatically. The 1630N10(R1) is a purpose-built horizontal machine with a direct-drive BT30 mechanical spindle and a 10-tool traveling ATC, eliminating chatter and reducing cycle time by over 40%.
Can the machine accommodate irregular weldments and oversized structural components?
Yes. The heavy-duty T-slot rotary table supports diverse custom fixtures and irregular weldments. For extra-long or wide structural fabrications exceeding standard table dimensions, modular auxiliary sub-tables can be mounted to provide stable outboard support without sacrificing rotary turnover capability.
What verified commercial milestone did the customer achieve with this machine?
Following commissioning, the machine operated continuously in full production for two continuous months with zero quality defects, zero tap breakage, and a verified 42% cycle time reduction. Based on these verified operational results, the customer issued an immediate formal repeat purchase order to expand production capacity.
DNC-1630N10(R1) 4-Axis CNC Horizontal Drilling & Tapping Machine — Specifications
Click to Expand Full Technical Specifications (17)
| Machine Model | DNC-1630N10(R1) |
| Machine Type | Horizontal 4-Axis CNC Drilling & Tapping Machine |
| X-axis Machining Stroke | 1600 mm |
| Y-axis Machining Stroke | 300 mm |
| Z-axis Machining Stroke | 600 mm |
| A-axis Rotary Platform | 360° Automatic Indexing |
| Spindle Type | High-Rigidity Taiwan Mechanical Spindle |
| Spindle Speed Range | 1000~6000 rpm Stepless Speed Regulation |
| Spindle Taper Hole | BT30 |
| Spindle Motor Power | 5.5 kW High-Torque Mechanical Spindle |
| Rapid Traverse Rates | X: 30–60 m/min, Y: 25 m/min, Z: 25 m/min |
| Tool Magazine Capacity | 10-Tool Traveling Servo Disc Magazine (Moves with Spindle) |
| Repeated Positioning Accuracy | ≤ 0.02 mm (API Laser Calibrated & Compensated) |
| Table Clamping Surface | Heavy-Duty T-Slot Rotary Table (Auxiliary Sub-Table Compatible) |
| Primary Machining Functions | Multi-Face Drilling, Synchronized Rigid Tapping, Slot Milling, Chamfering |
| Machining Capacity Range | Drilling Ø1–Ø20 mm | Synchronized Rigid Tapping M3–M18 |
| Safety & Quality Standard | CE Certified |
Request a Free Sample Machining & Feasibility Analysis
Send your tube dimensions, material grade, and thread specifications. Our tooling engineers will verify feasibility, calculate cycle time, and run a live machining test on your spec.